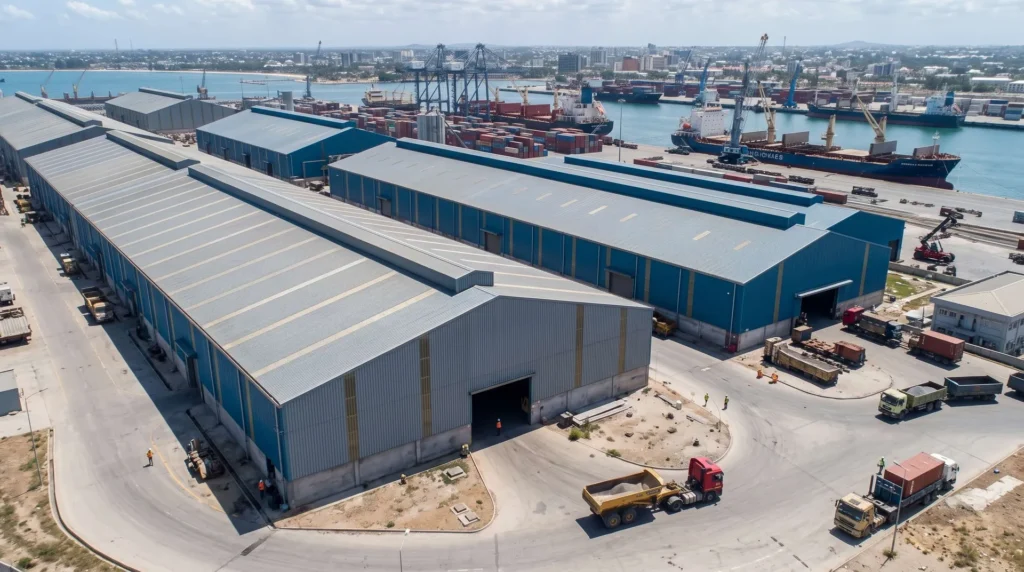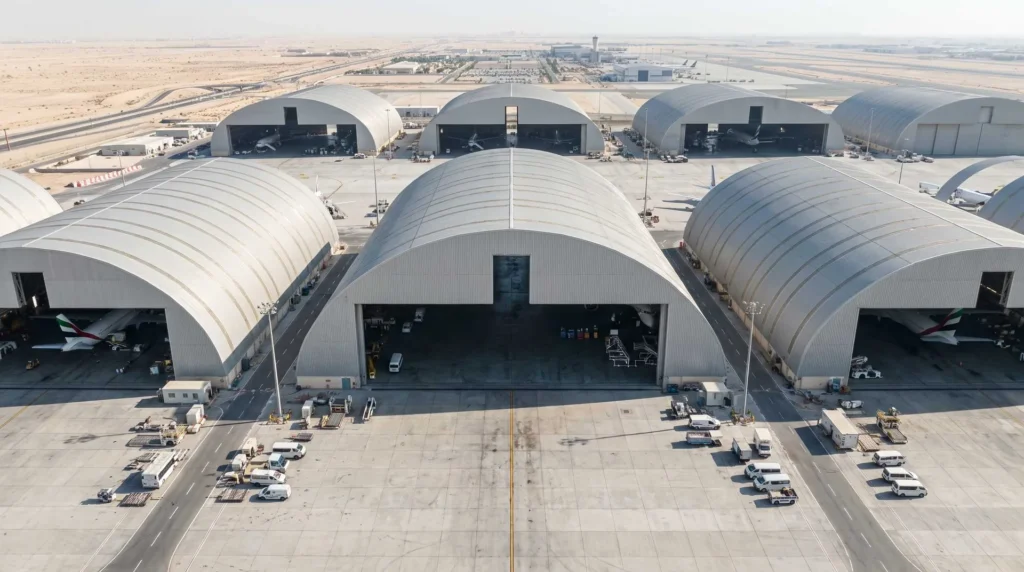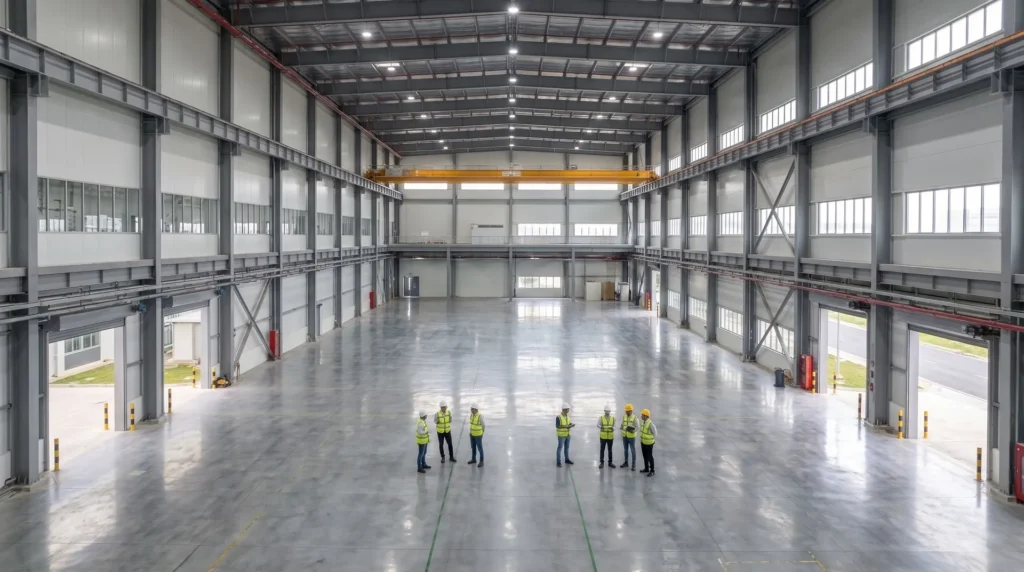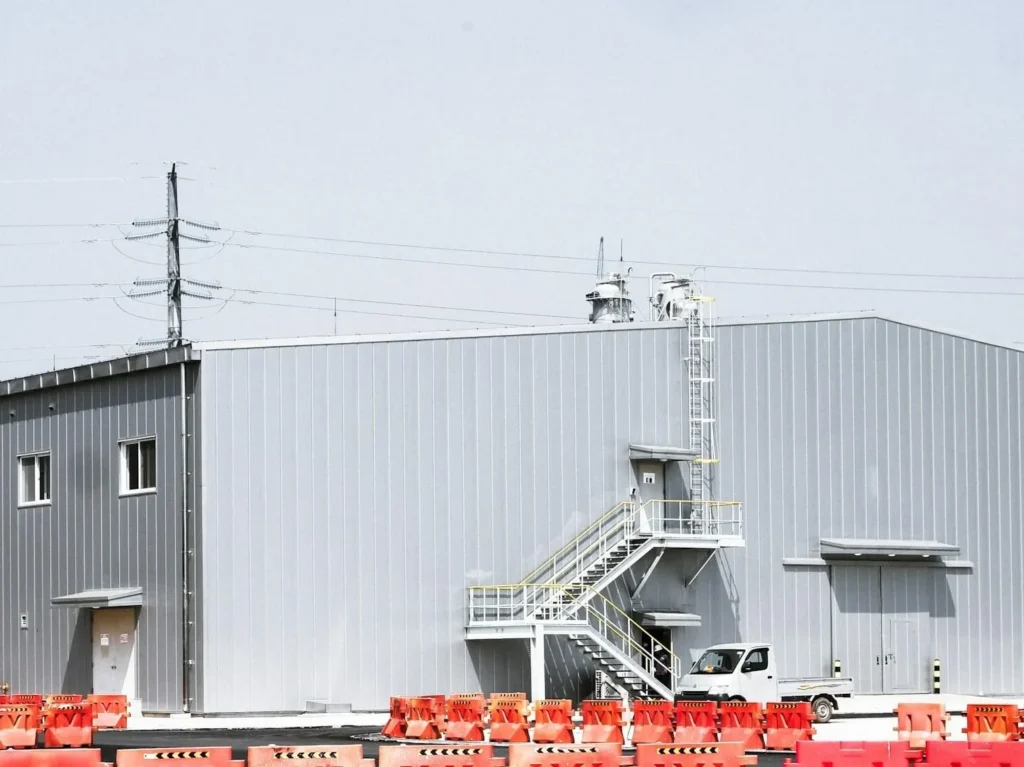
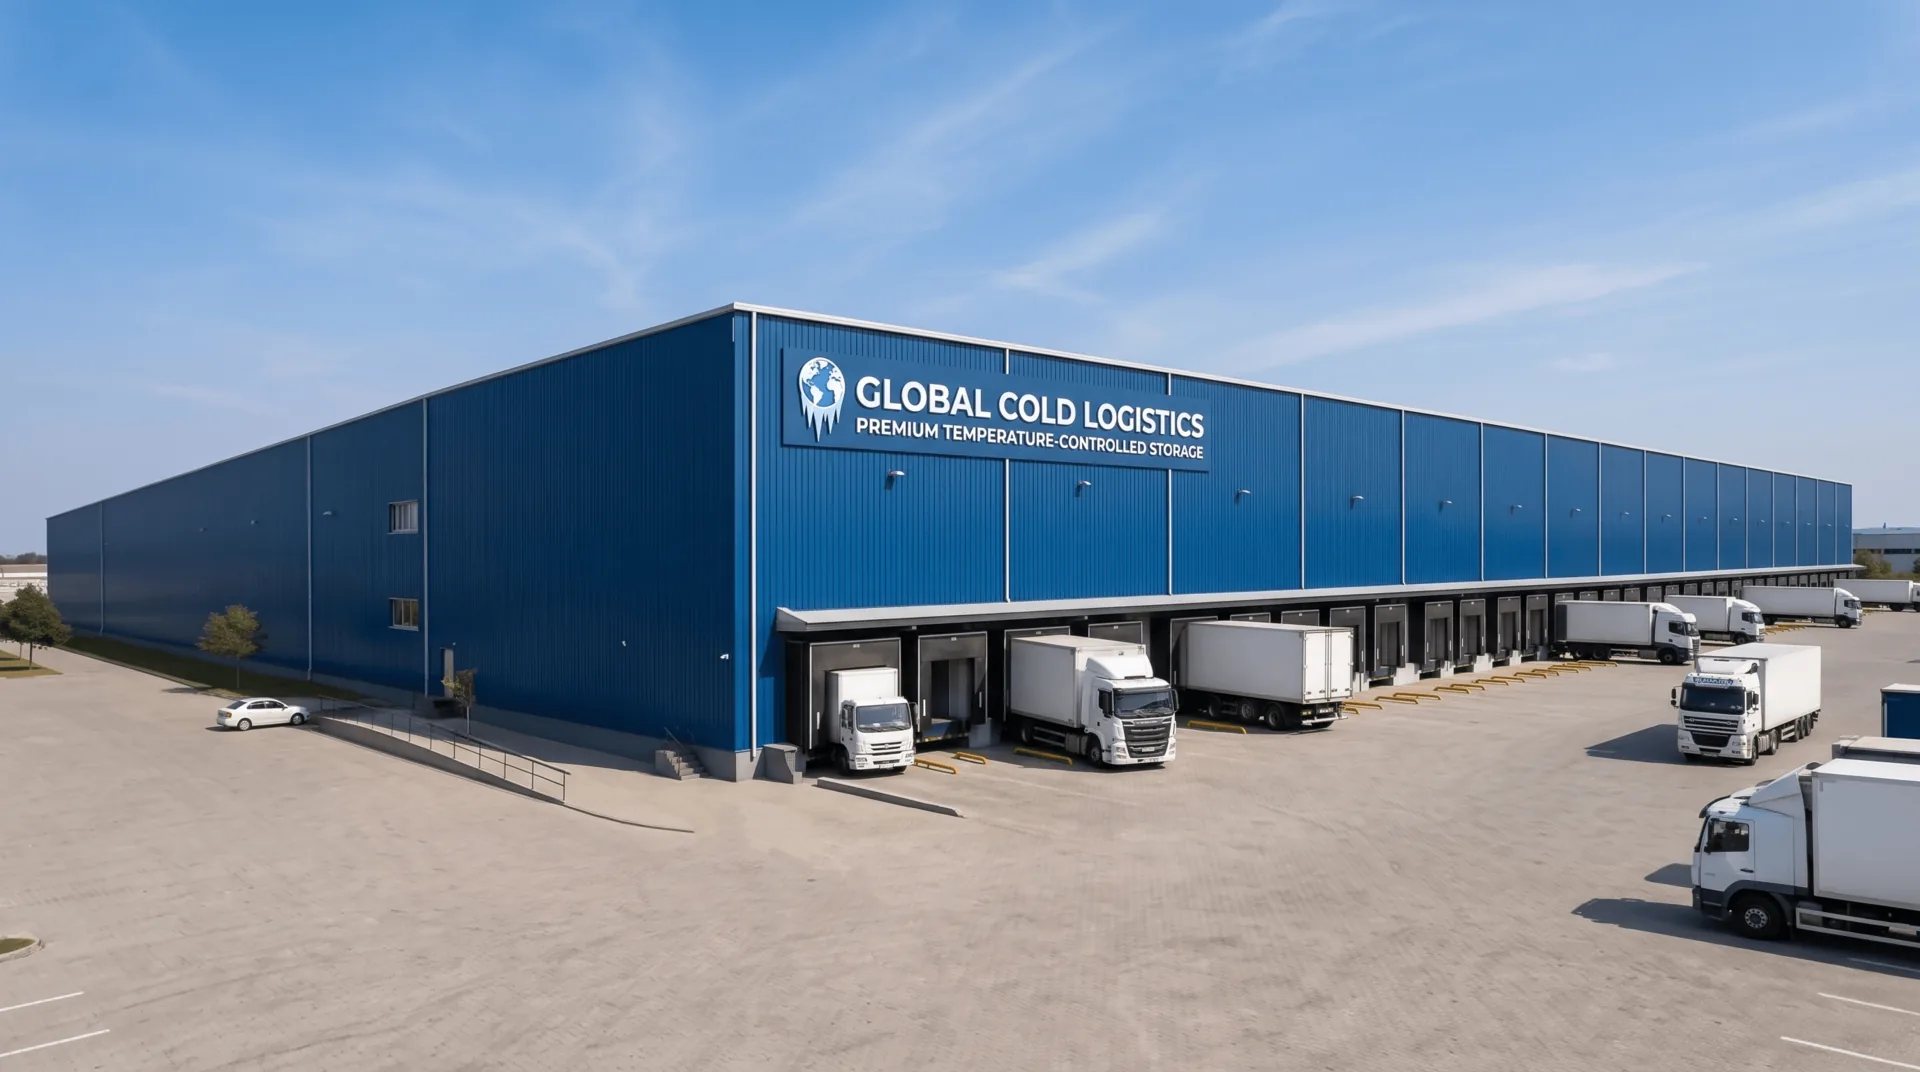
Prefabricated Steel Warehouse
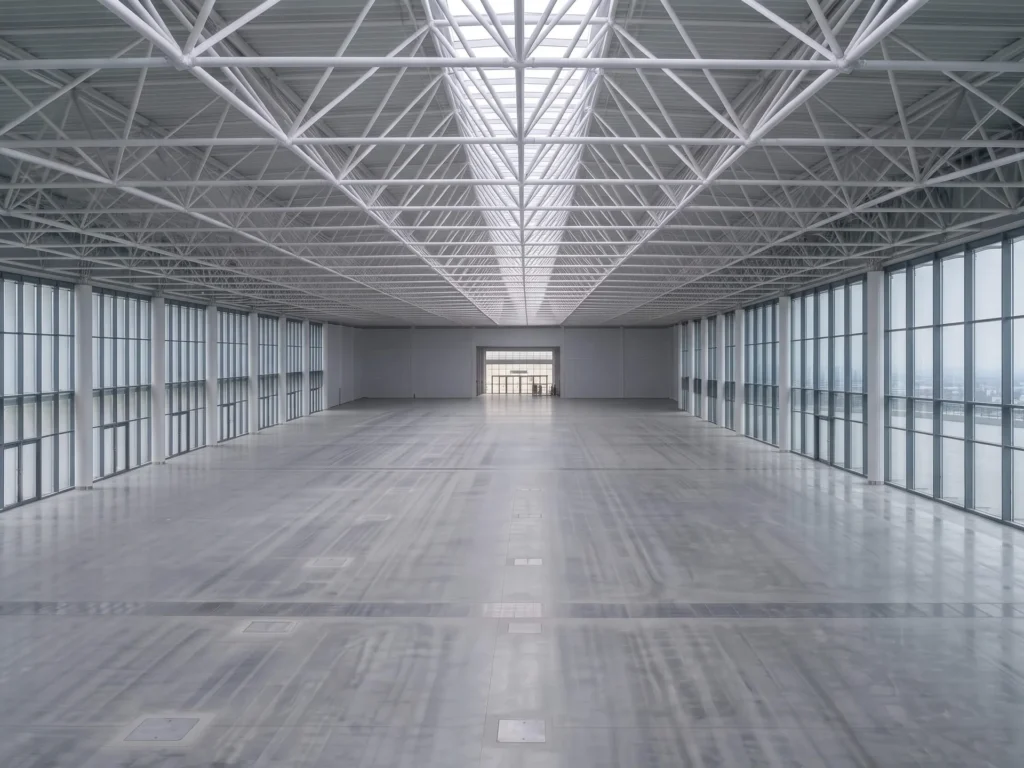
100m+ Clear Span | 30% CAPEX Reduction | Standardized Shipping
READY TO BUILT.
ZERO REWORK
01 / 06
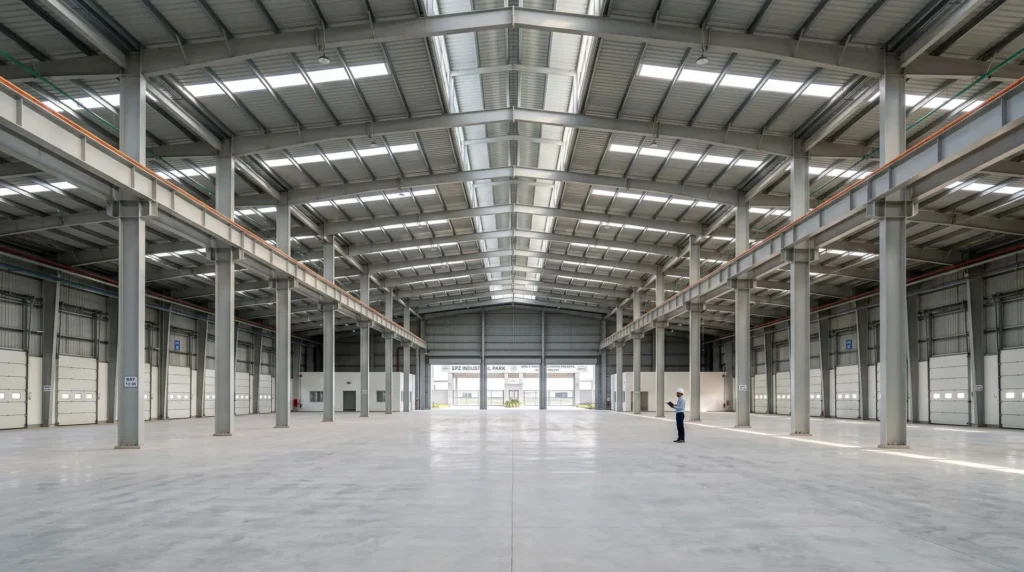
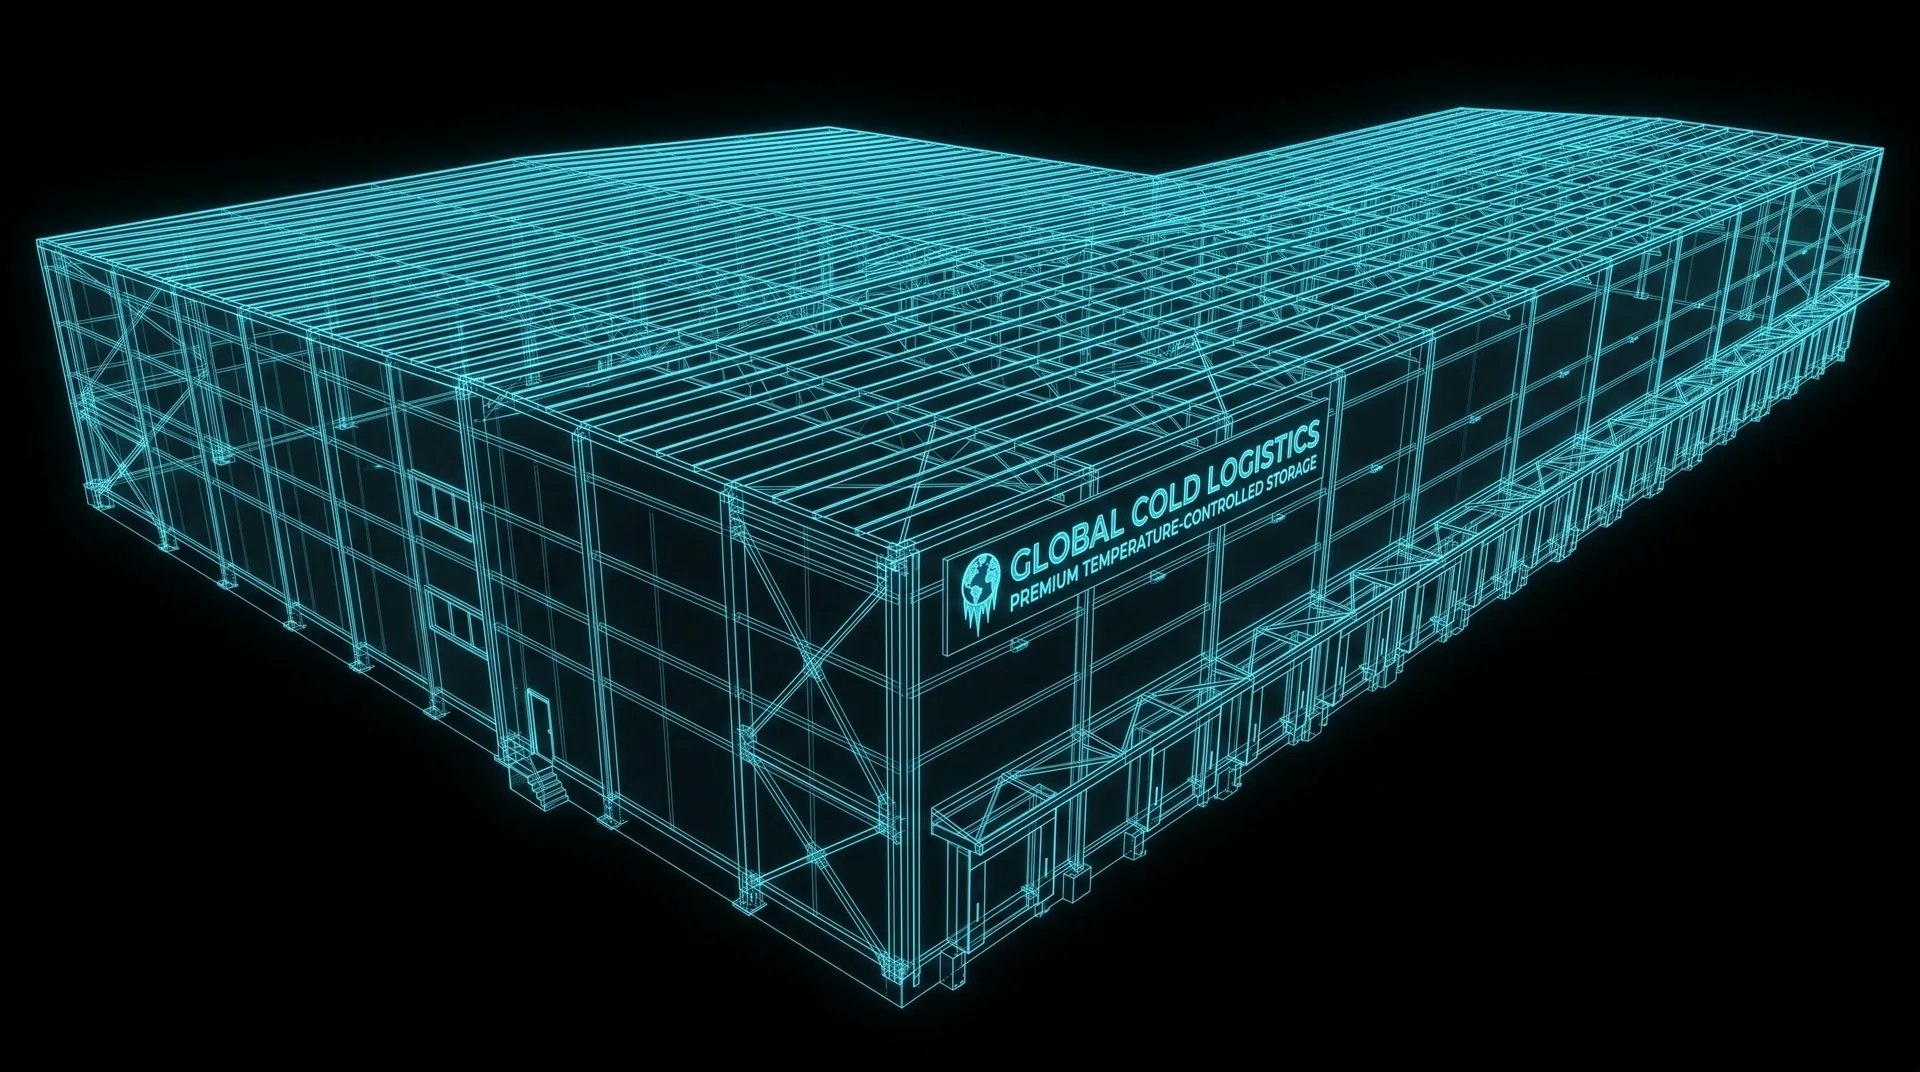
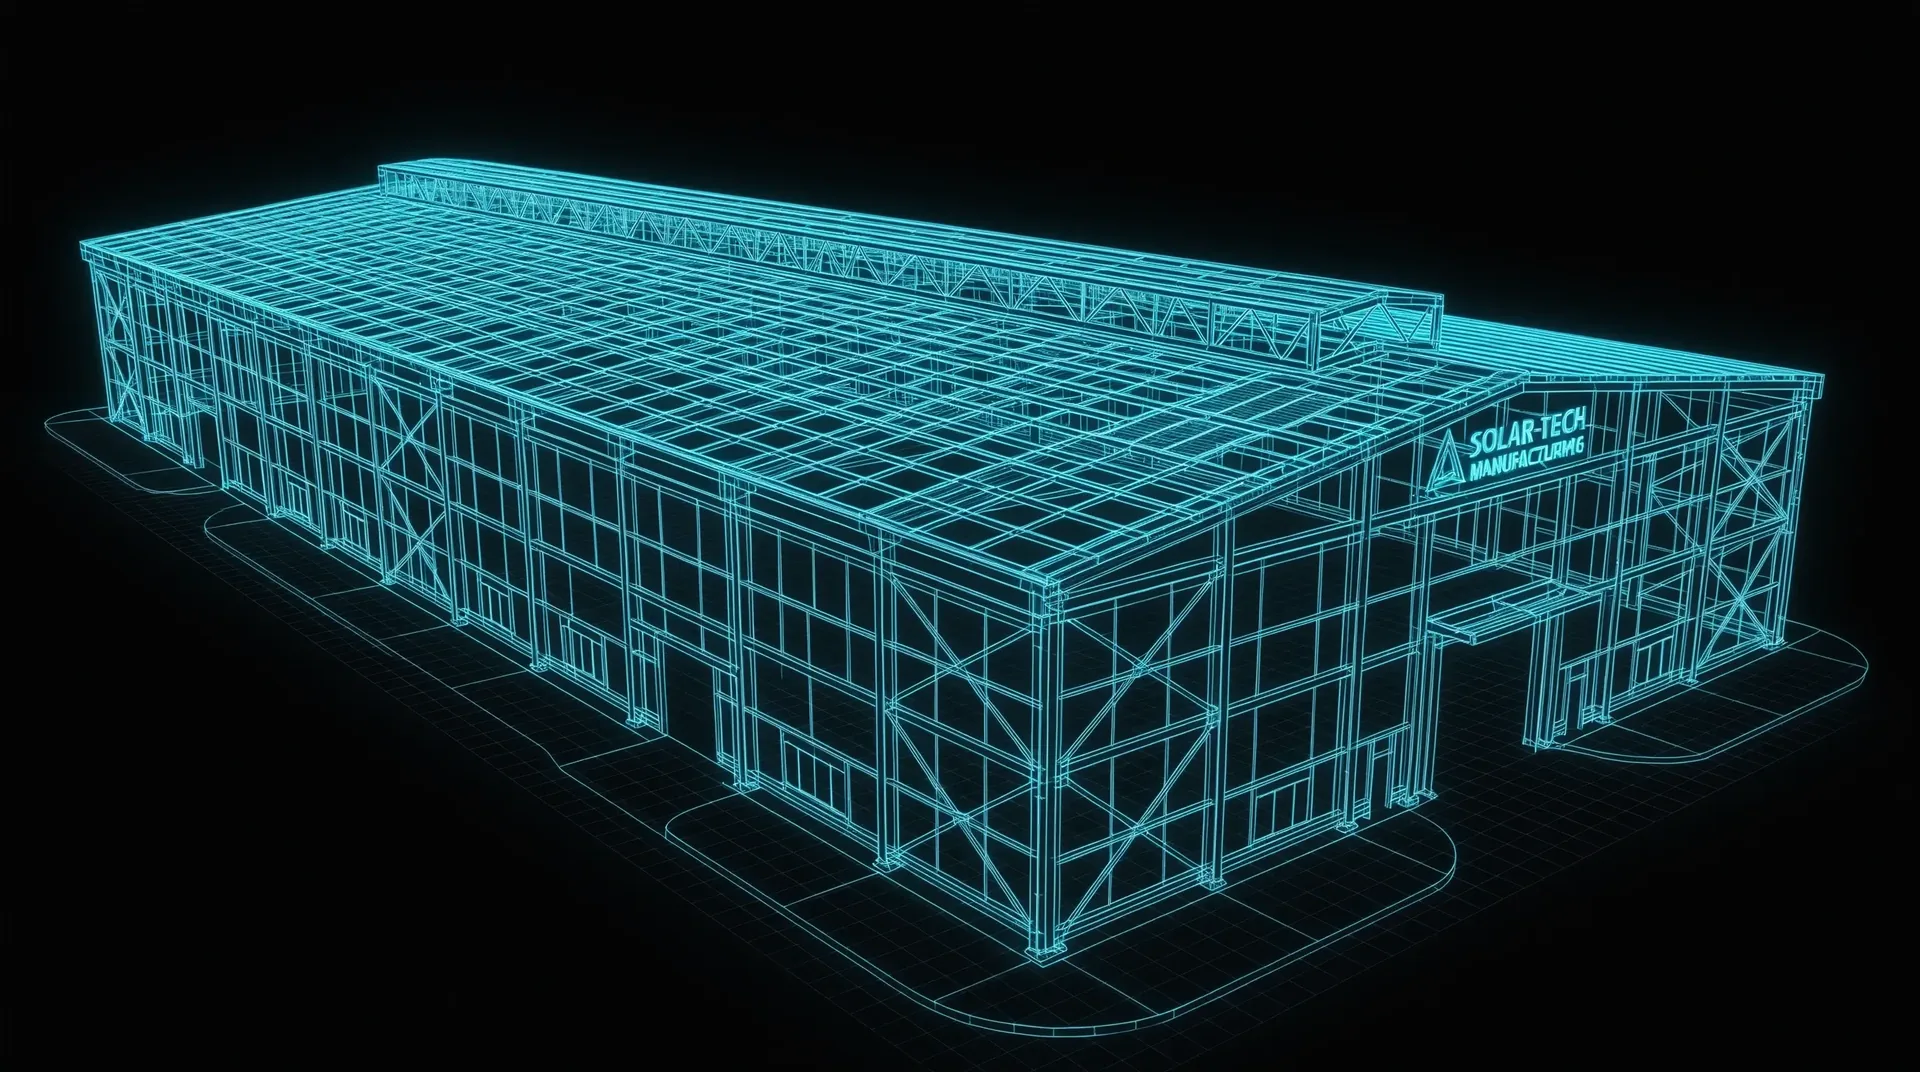
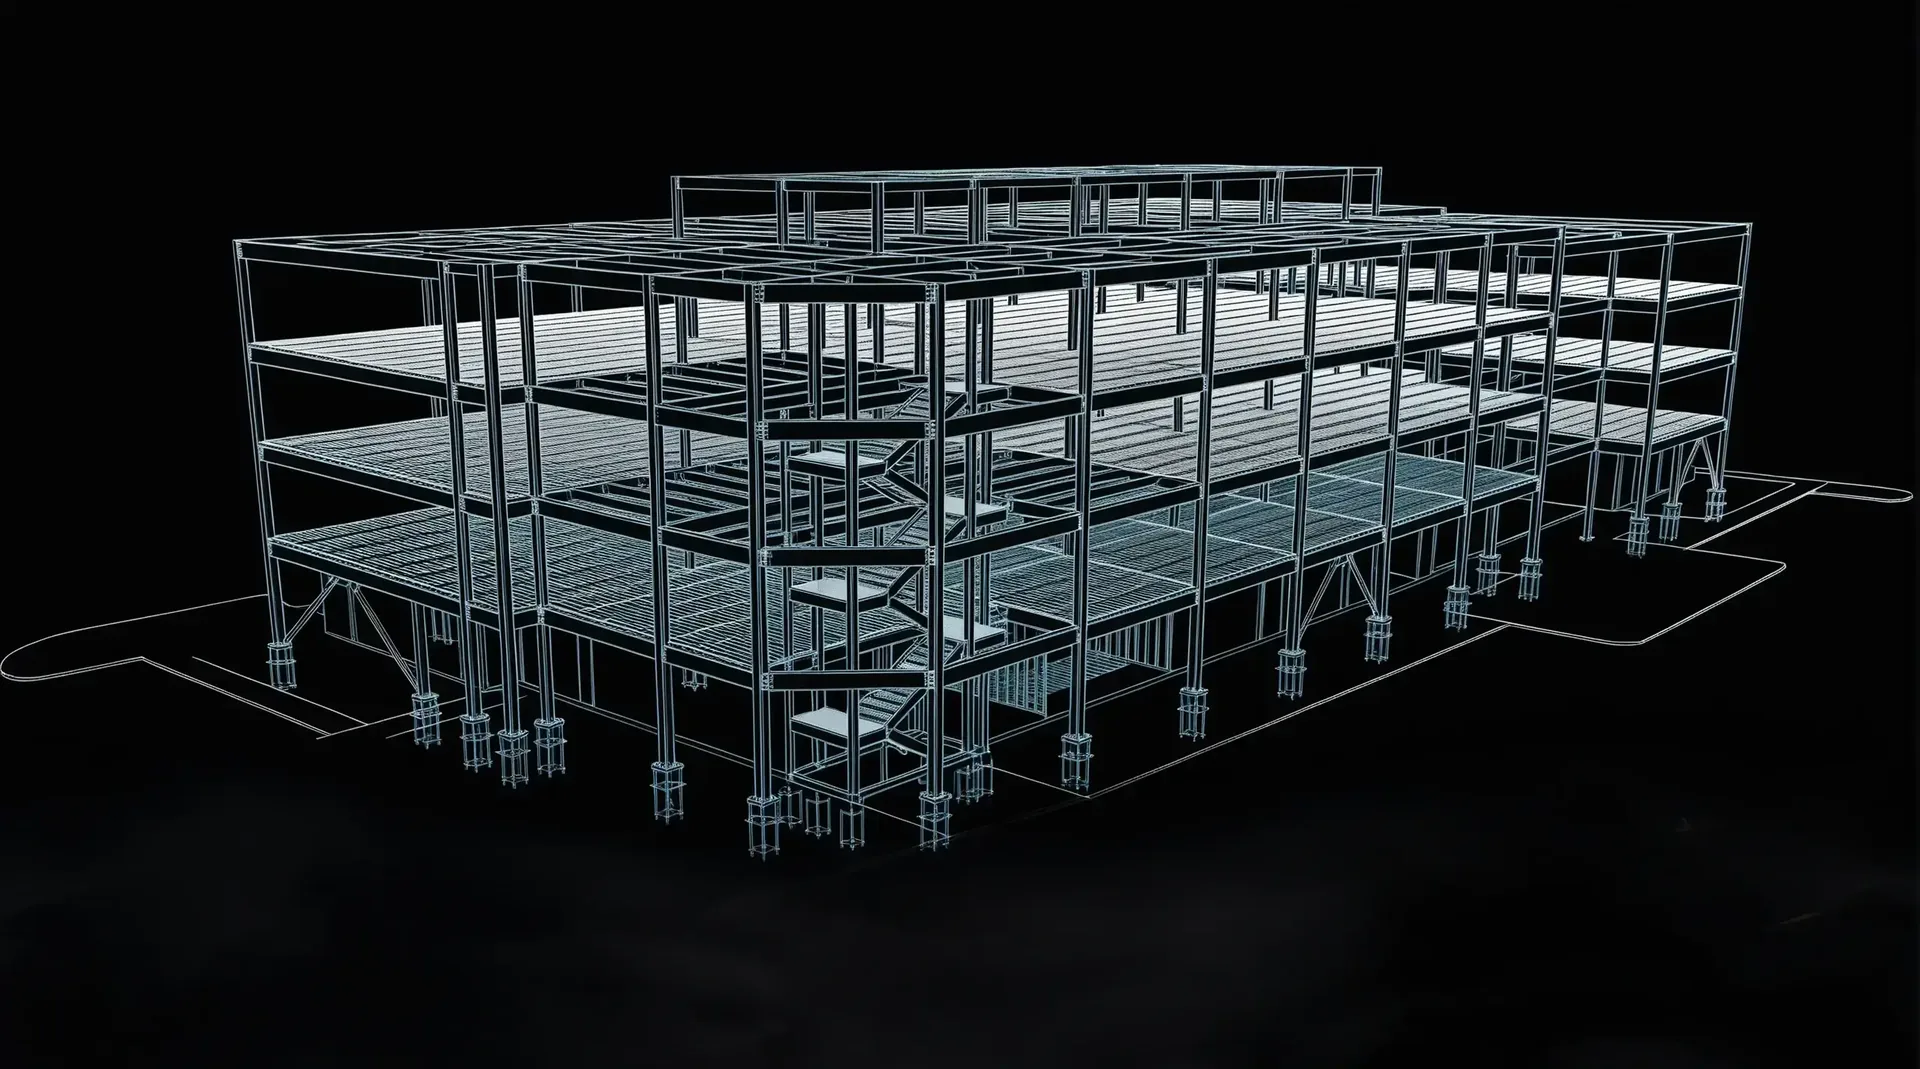
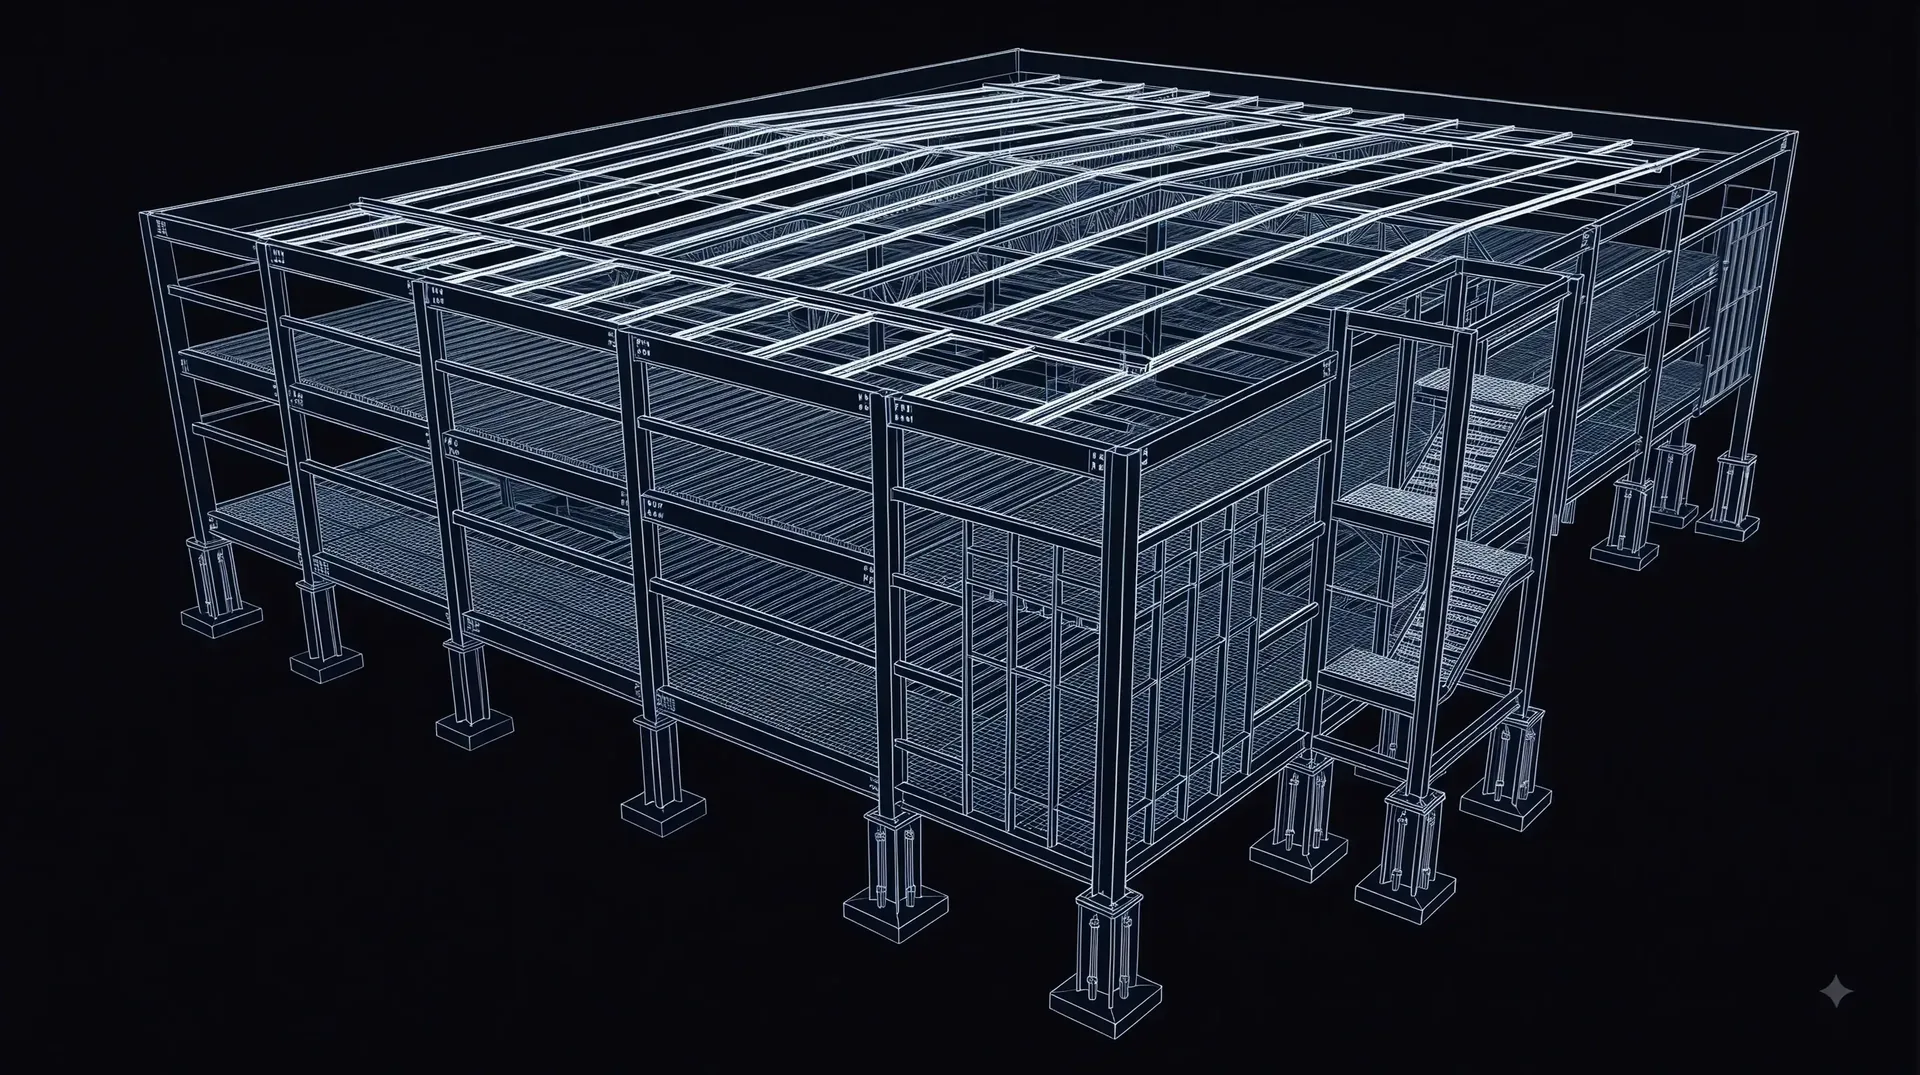
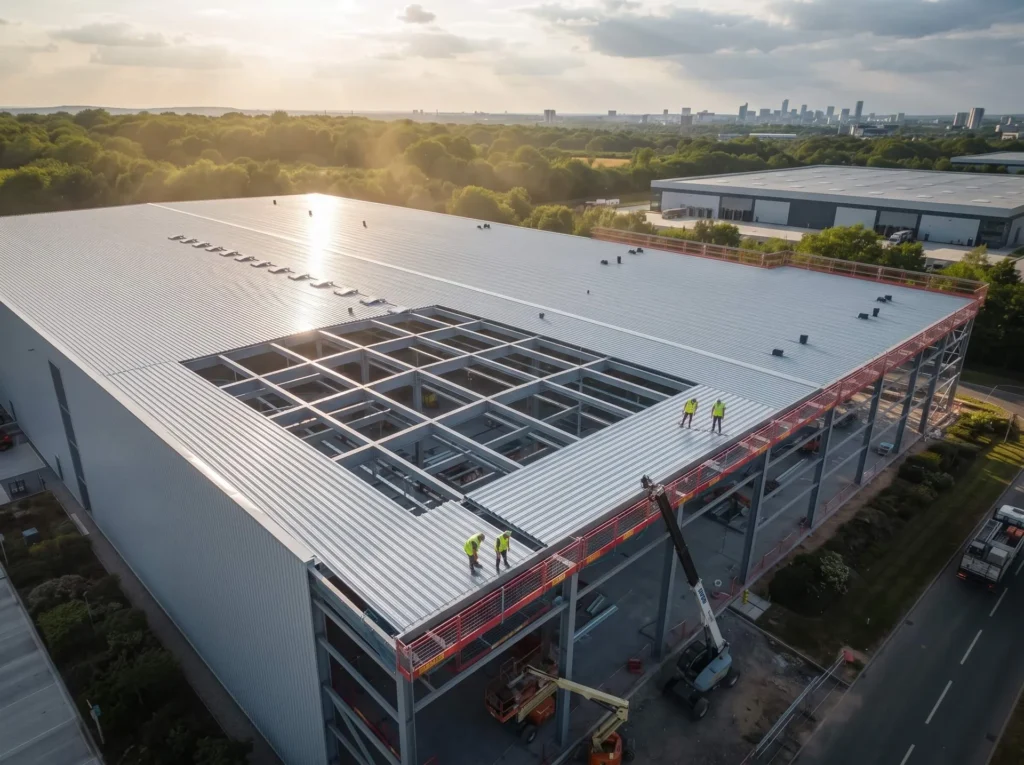
Portal Frame Structure
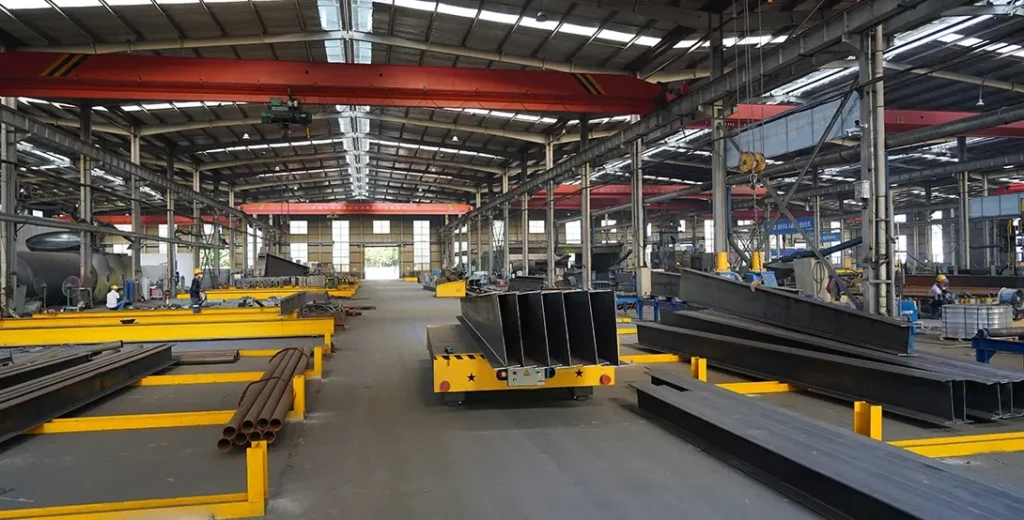
SynJect PEB deliver rapid deployment and maximum ROI through BIM-optimized detailing. Millimeter-accurate, factory-fabricated components guarantee seamless on-site assembly, eliminating rework and accelerating your industrial project timeline with dependable consistency.
Qualification Certificate
Your projects are protected by world-class standards. From CE (EN 1090) to ISO 9001, our qualifications are not just paper—they are the rigorous daily reality on our shop floor.
ISO 9001 Quality Management System
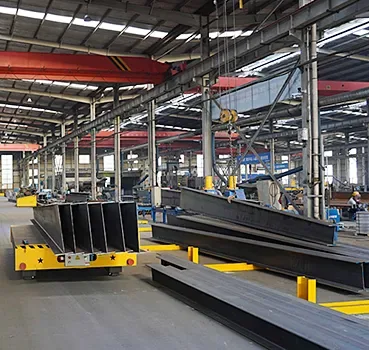
From Blueprint to Site. Zero Friction.
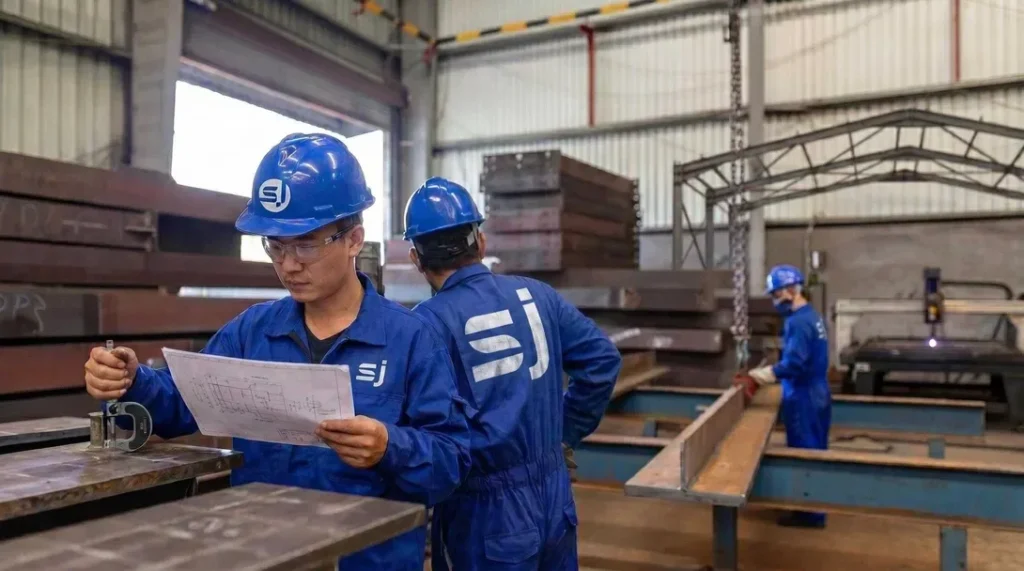
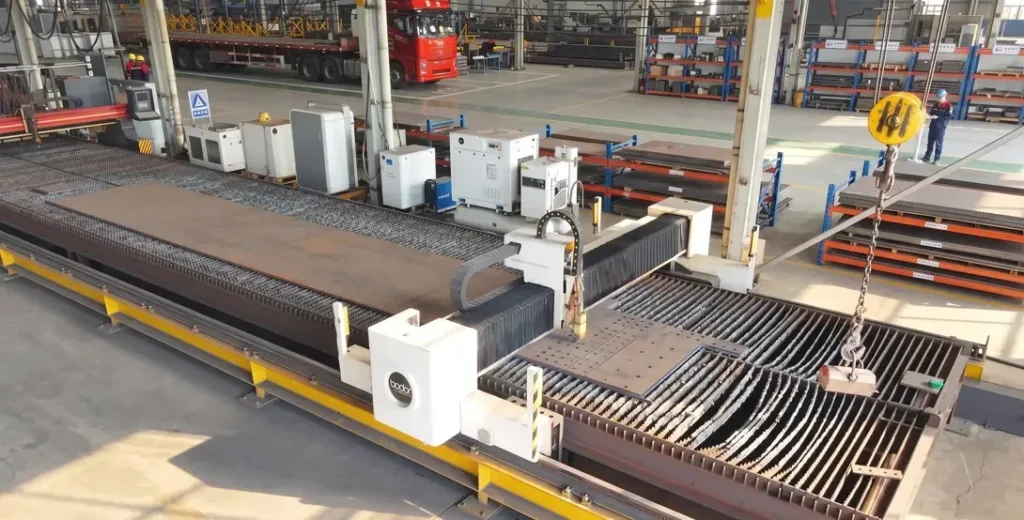
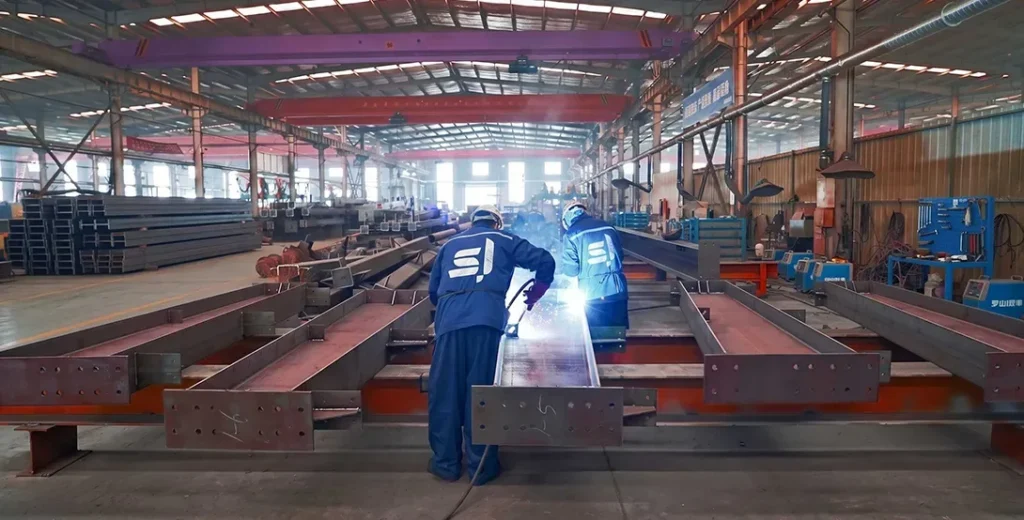
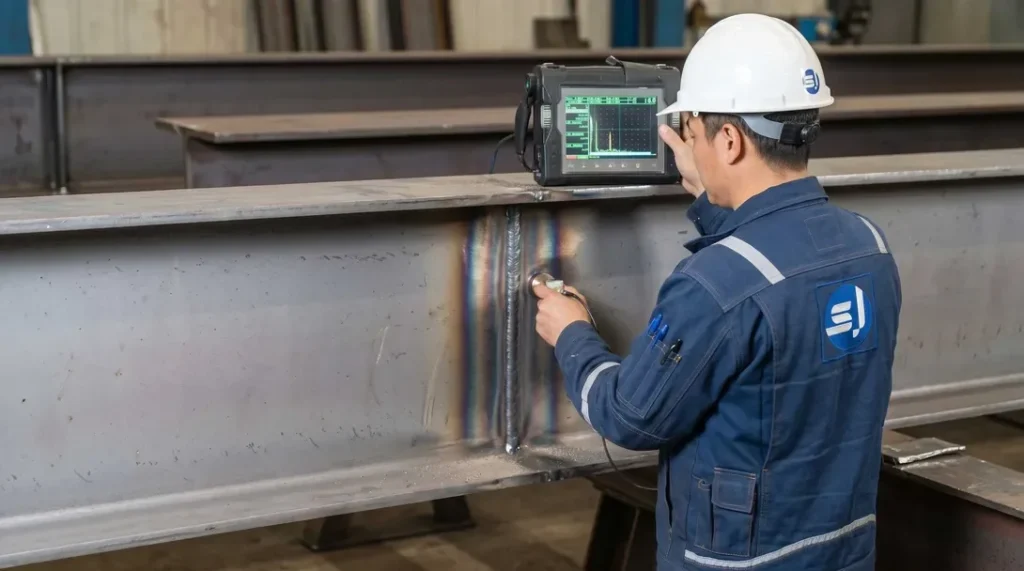
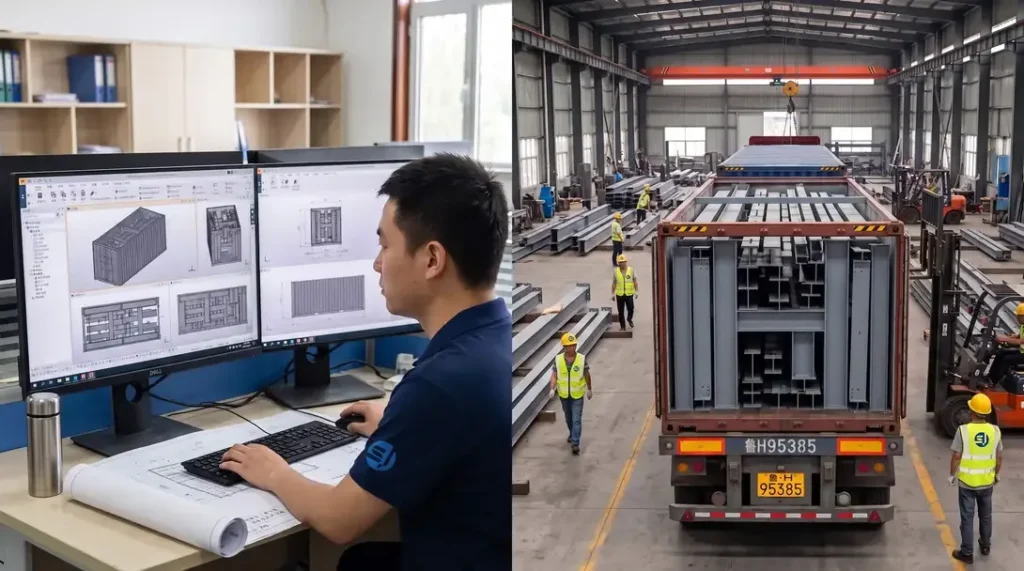
Stage.01
Detailed Engineering
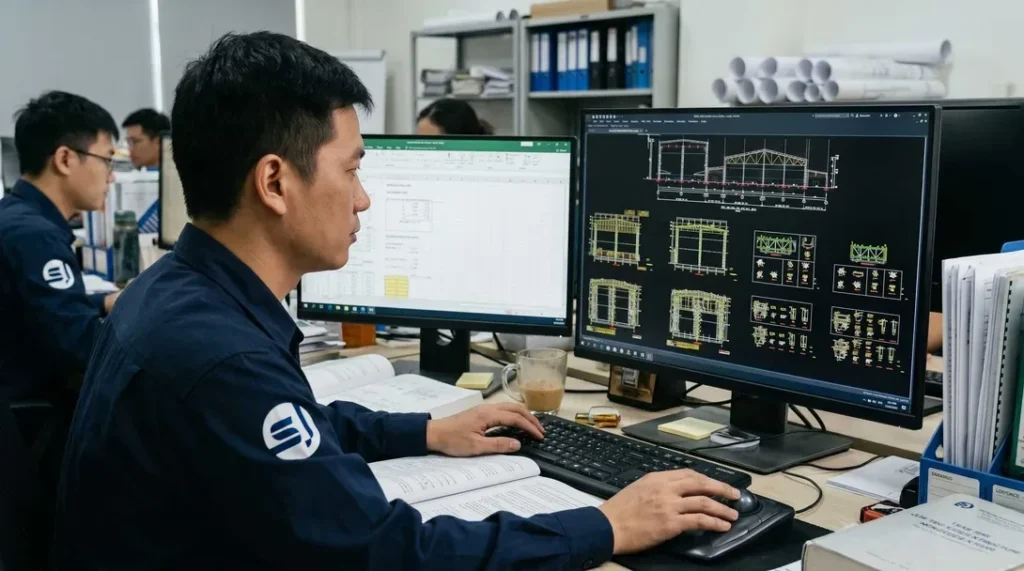
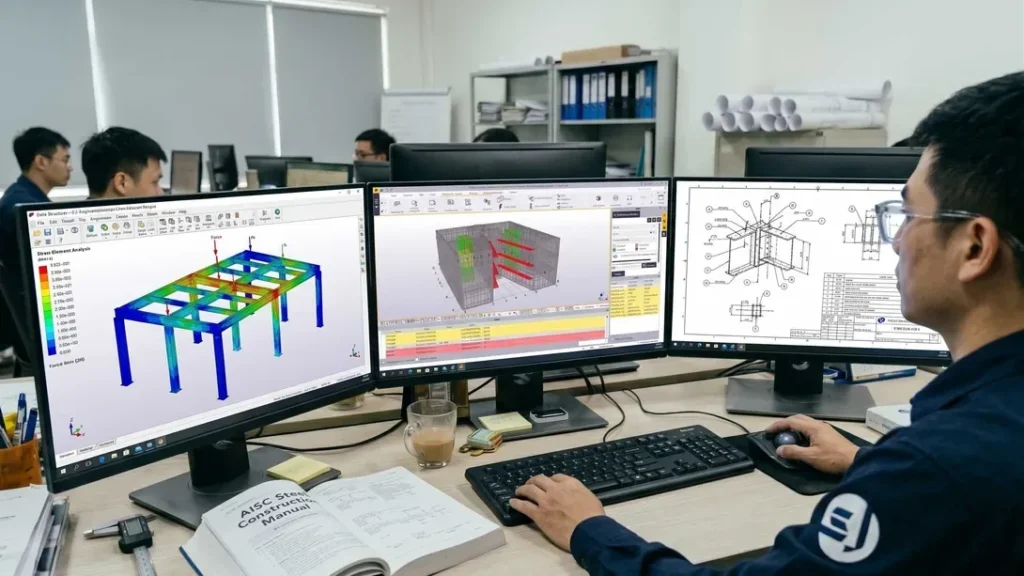
Utilizing advanced BIM platforms such as Tekla Structures, detailed 3D modeling and shop drawings are executed strictly in compliance with AISC 360 or Eurocode 3 (EN 1993). Connection designs are rigorously verified, with manufacturing drawings generated to ISO 2768-m tolerance standards. 100% clash detection with primary architectural and MEP systems is performed to ensure zero structural conflicts during field erection.
STANDARDAISC 360 / EN 1993
METRIC VALUETolerance ±0.01mm
Stage.02
Nesting & Material Optimization
Intelligent nesting layouts are performed using advanced software like FastCAM/SigmaNEST in accordance with EN 10029 / ASTM A6 dimensional standards. Accounting for cutting kerf (2mm–5mm depending on plate thickness) and thermal contraction allowances, raw material utilization exceeds 92%. Offcuts are digitally barcode-tracked to ensure 100% mill test report (MTR) traceability.
STANDARDEN 10029 / ASTM A6
METRIC VALUEUtilization 95%
Stage.03
Raw Material Incoming Inspection
All structural steel (Q355B/C/D, ASTM A572 Gr.50, S355JR/J2) must be accompanied by EN 10204 3.1 Mill Test Reports (MTR). Incoming quality control conducts 100% dimensional and visual inspections under ASTM A6 / EN 10029, verifying thickness tolerances (Class A/B) and internal lamination integrity via Ultrasonic Testing (UT) to ASTM A435. Chemical composition and mechanical properties are spot-verified by accredited 3rd-party labs.
STANDARDEN 10204 3.1 / ASTM A435
METRIC VALUEClass A/B and ASTM A435
Stage.04
CNC Cutting & Edge Preparation
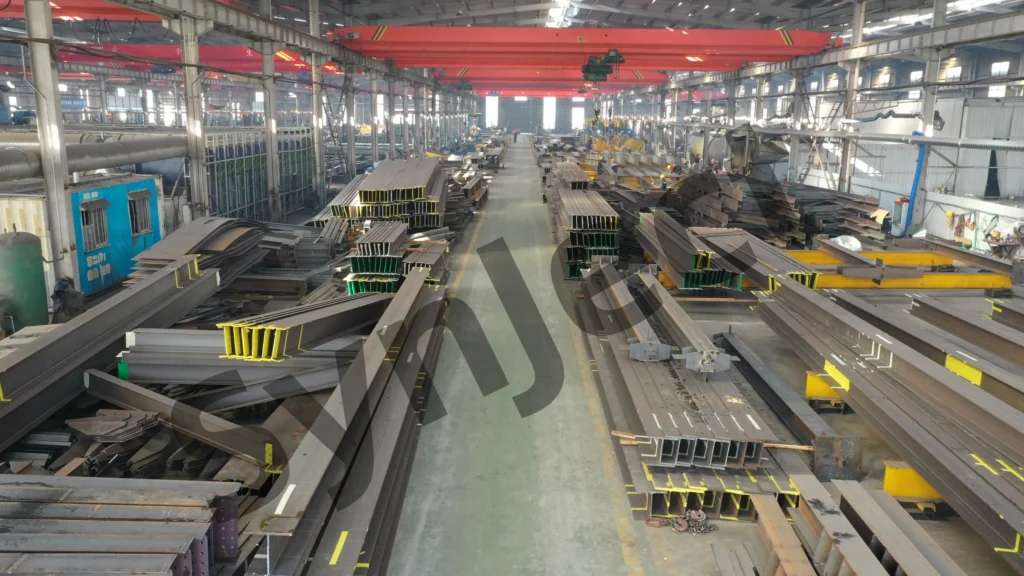
Plate profiling and component cutting are executed via CNC oxy-fuel, high-definition plasma, and multi-kW fiber laser equipment. Cut surface quality strictly complies with EN ISO 9013 for perpendicularity and surface roughness ±2.5°, Range 3/4 tolerance). Multi-axis CNC beveling machines execute weld prep bevel angles within ±2.5° and root face dimensions within ±1.0 mm.
STANDARDEN ISO 9013
METRIC VALUERa ≤12.5μm
Stage.05
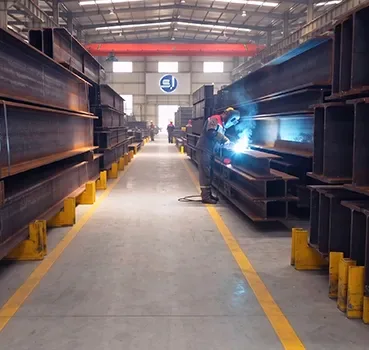
Primary Structural Welding
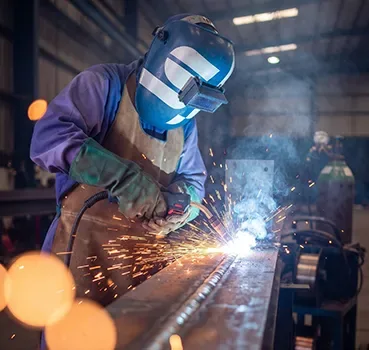
Welding is performed exclusively by AWS D1.1 or EN ISO 9606 certified welders using qualified Welding Procedure Specifications (WPS) supported by Procedure Qualification Records (PQR) per AWS D1.1 / ISO 15614. Submerged Arc Welding (SAW) and Flux-Cored Arc Welding (FCAW) dominate Complete Joint Penetration (CJP) and fillet welds. Heat input is strictly controlled, achieving weld quality levels conforming to ISO 5817 Quality Level B or AWS D1.1 standards.
STANDARDAWS D1.1 / EN ISO 9606
METRIC VALUEISO 5817Level B
Stage.06
Weld Distortion Straightening
Post-weld angular distortion, camber, and sweep are rectified using automated hydraulic flange straighteners and controlled thermal flame straightening. Heating temperatures for High-Strength Low-Alloy (HSLA) steels are strictly maintained between 600℃ - 650℃ (air-cooled, zero water quenching) to prevent microstructural degradation. Post-straightening straightness tolerances meet ±3 mm, conforming to EN 1090-2 Execution Class 2 (EXC2/EXC3) and AISC COSP standards.
STANDARDEN 1090-2 EXC2 / AISC COSP
METRIC VALUETolerances ±3 mm
Stage.07
Non-Destructive Testing (NDT)
NDT protocols are operated by ISO 9712 / ASNT Level II certified NDT personnel. 100% of critical Complete Joint Penetration (CJP) welds undergo Ultrasonic Testing (UT per ISO 17640 / ASTM E164) or Magnetic Particle Testing (MT per ISO 17638 / ASTM E709). Radiographic Testing (RT) is applied as requested for heavy sections. Weld acceptance conforms strictly to ISO 11666 Acceptance Level 1 or AWS D1.1 criteria.
STANDARDISO 11666 Level 1 / AWS D1.1
METRIC VALUE100% UT
Stage.08
Trial Assembly & Shop Alignment
Complex geometries, long-span trusses, and heavy framing undergo 1:1 physical trial assembly or high-precision 3D laser scanning virtual assembly per EN 1090-2 / AISC requirements. Bolt hole alignment is verified (≥ 95% free-pass rate for high-strength bolts), and critical dimensions (span, camber, 3D spatial alignment) are verified within tight tolerance limits (±2.0 mm) to eliminate site fitting risks.
STANDARDAISC / EN 1090-2
METRIC VALUETolerance ±2.0 mm
Stage.09
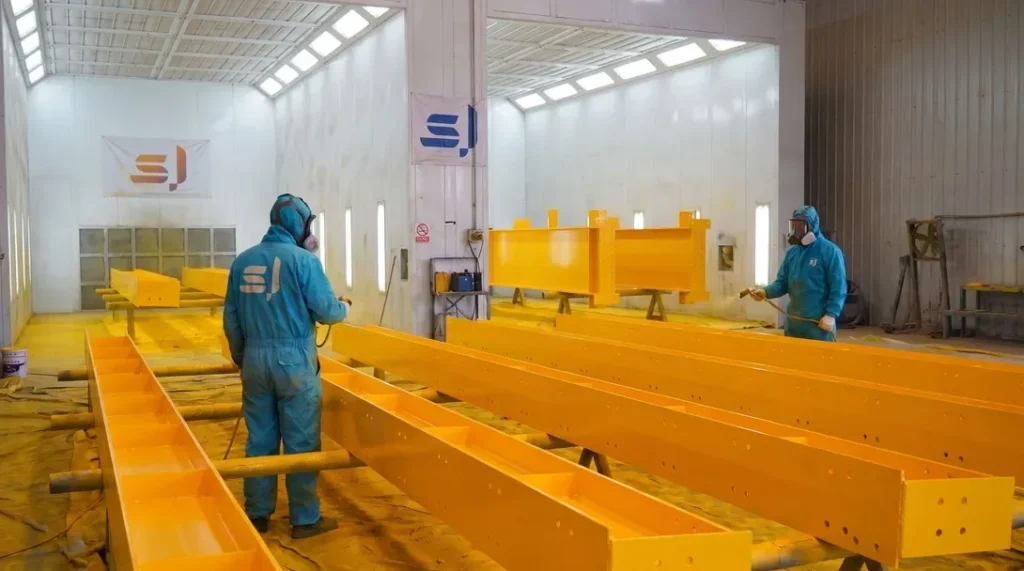
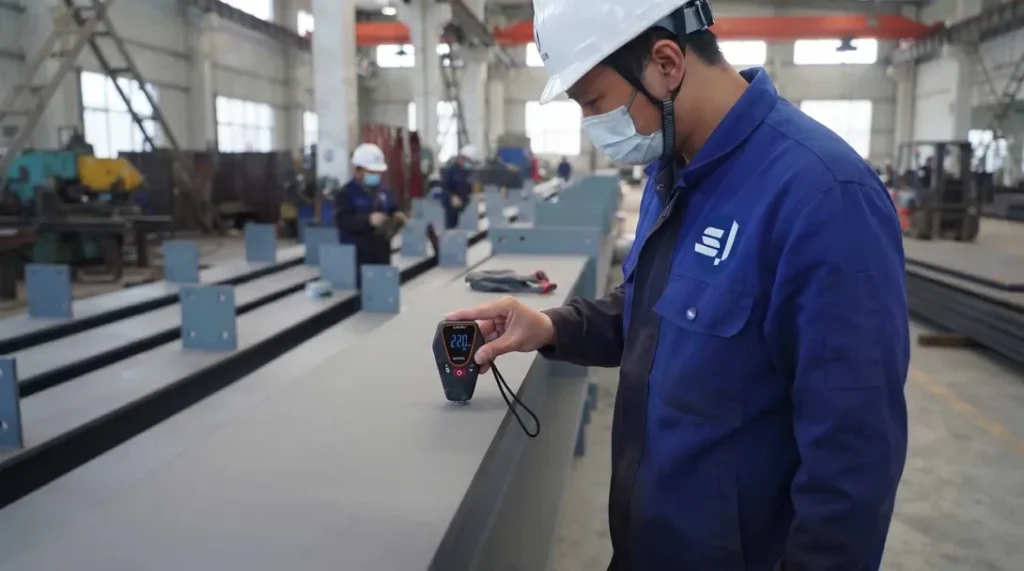
Surface Preparation & Protective Coating
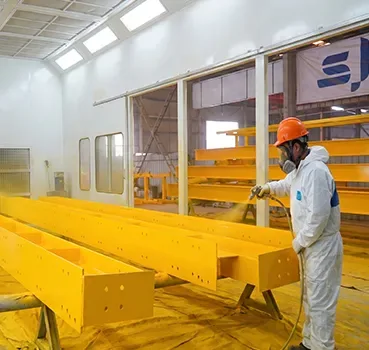
Structural members undergo automated shot blasting to achieve SSPC-SP10 / NACE No. 2 / ISO 8501-1 Sa 2.5 cleanliness, with a surface profile (anchor depth) of 45–75μm. High-performance protective coatings are applied using airless spray technology in compliance with ISO 12944 (C3 to CX corrosive environments), featuring Inorganic/Organic Zinc-Rich Epoxy Primers, Epoxy Micaceous Iron Oxide Intermediate coats, and Polyurethane/Fluorocarbon Topcoats. Dry Film Thickness (DFT) is verified using calibrated magnetic gauges adhering strictly to the 90/10 rule.
STANDARDISO 8501-1 Sa 2.5 / ISO 12944
METRIC VALUE45 - 75μm
Stage.10
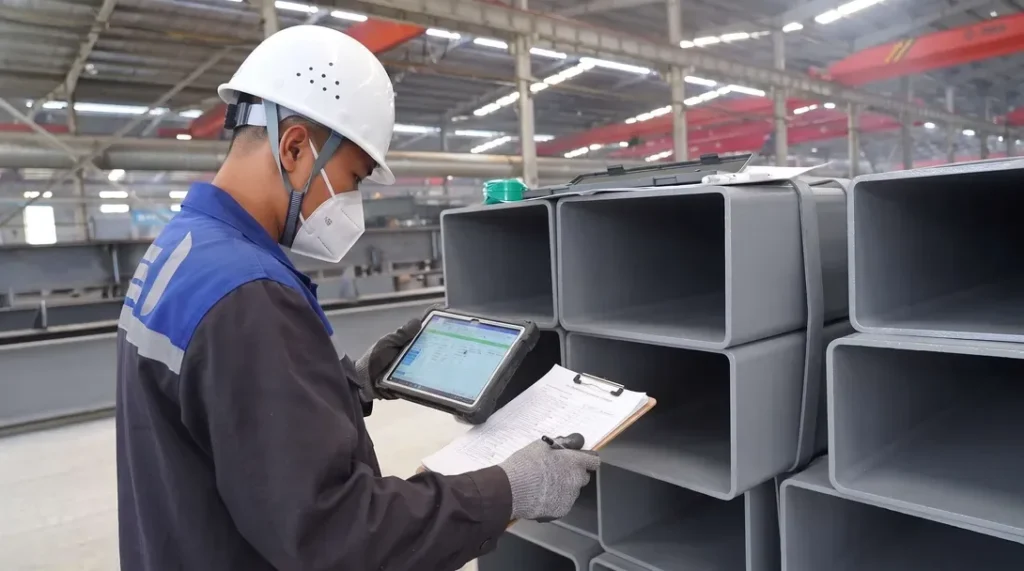
Final Quality Inspection & Certification
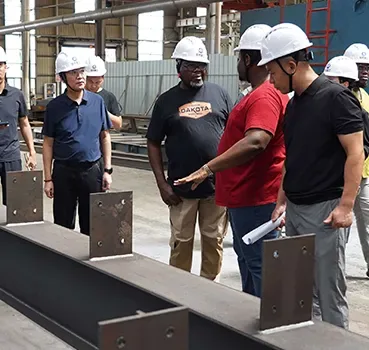
Final Quality Control (FQC) performs a comprehensive holistic audit, inspecting paint aesthetics (zero runs, pinholes, sagging), critical geometry, bolt hole pitches, and laser/stenciled component mark traceability. A complete Manufacturing Data Report (MDR)—comprising MTRs, NDT records, coating inspection logs, and Certificates of Conformance—is compiled to support CE Marking (DoP under EN 1090) and AISC final acceptance.
STANDARDEN 1090 / AISC
METRIC VALUEQA/QC Final Release
Stage.11
Export Packaging & Logistics Protection
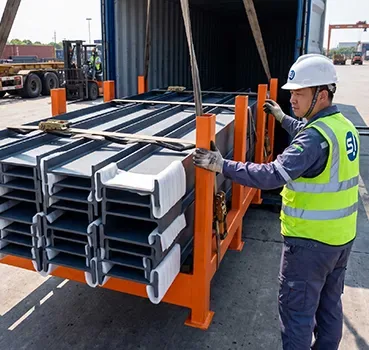
Protective packaging is engineered for containerized (40HQ/OT/FR) and breakbulk ocean freight under heavy maritime transit conditions. Structural members are bundled on heavy-duty steel skids with high-tensile steel strapping. Machined connections and contact surfaces are wrapped with VCI anti-corrosion film, EPE foam padding, and heavy rubber cushions. All timber packing complies fully with ISPM 15 phytosanitary standards and IMO Cargo Stowage and Securing (CSS) rules.
STANDARDISPM 15 / IMO CSS
METRIC VALUE40HQ/OT/FR
Stage.12
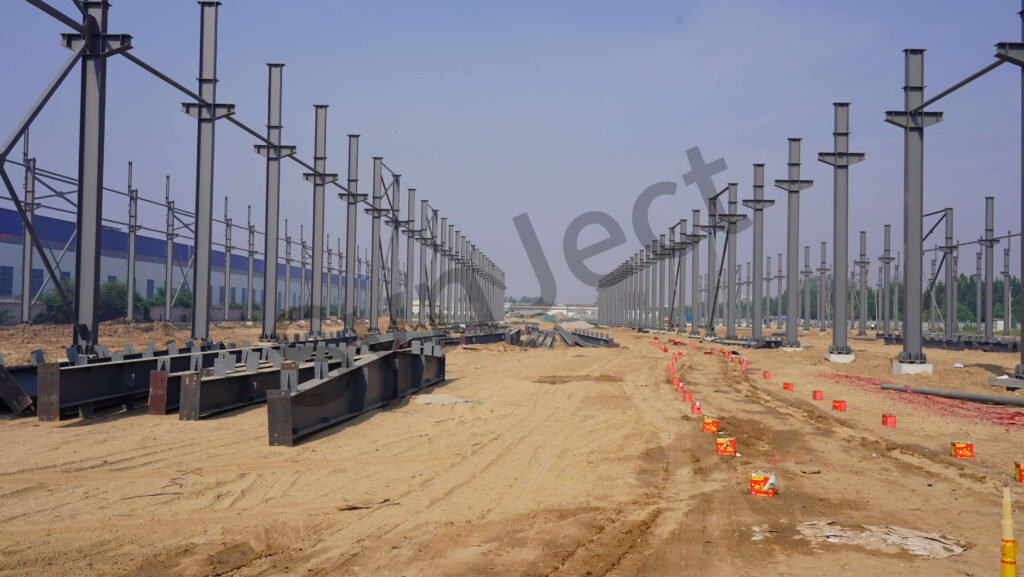
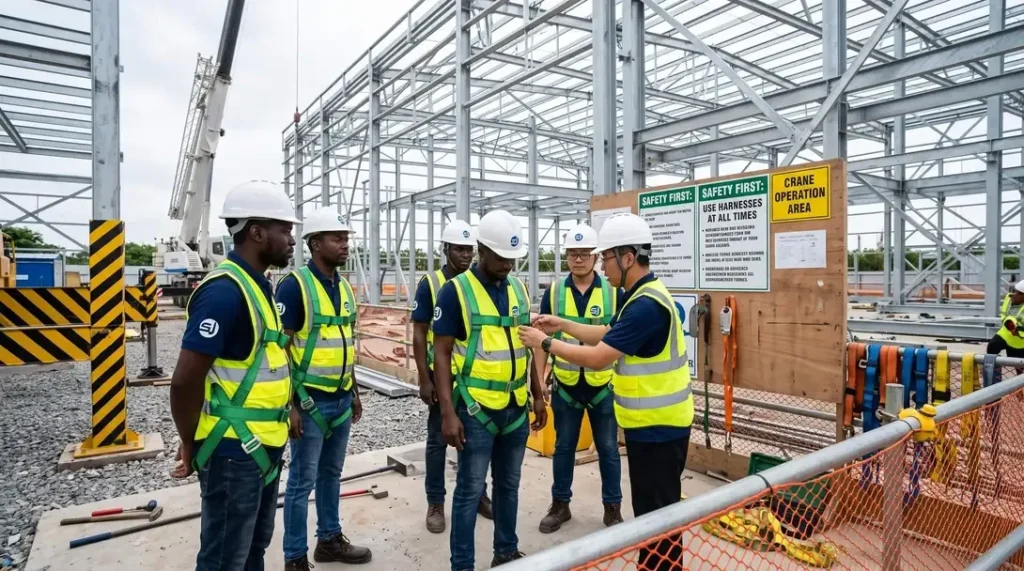
Global Field Erection & Site Management
We deliver international site erection supervision and turnkey EPCM construction services adhering to OSHA 1926 safety protocols, AISC COSP, and EN 1090-2 erection standards. Field teams, led by multilingual HSE and QA/QC engineers, utilize high-precision total stations to maintain structural plumbness within H/1000$ (≤25mm max). High-Strength Structural Bolting is executed via calibrated Wrench or Turn-of-Nut methods with 100% torque audit documentation.
STANDARDOSHA 1926 / EN 1090-2
METRIC VALUE≤ H/1000
GLOBAL DELIVERY
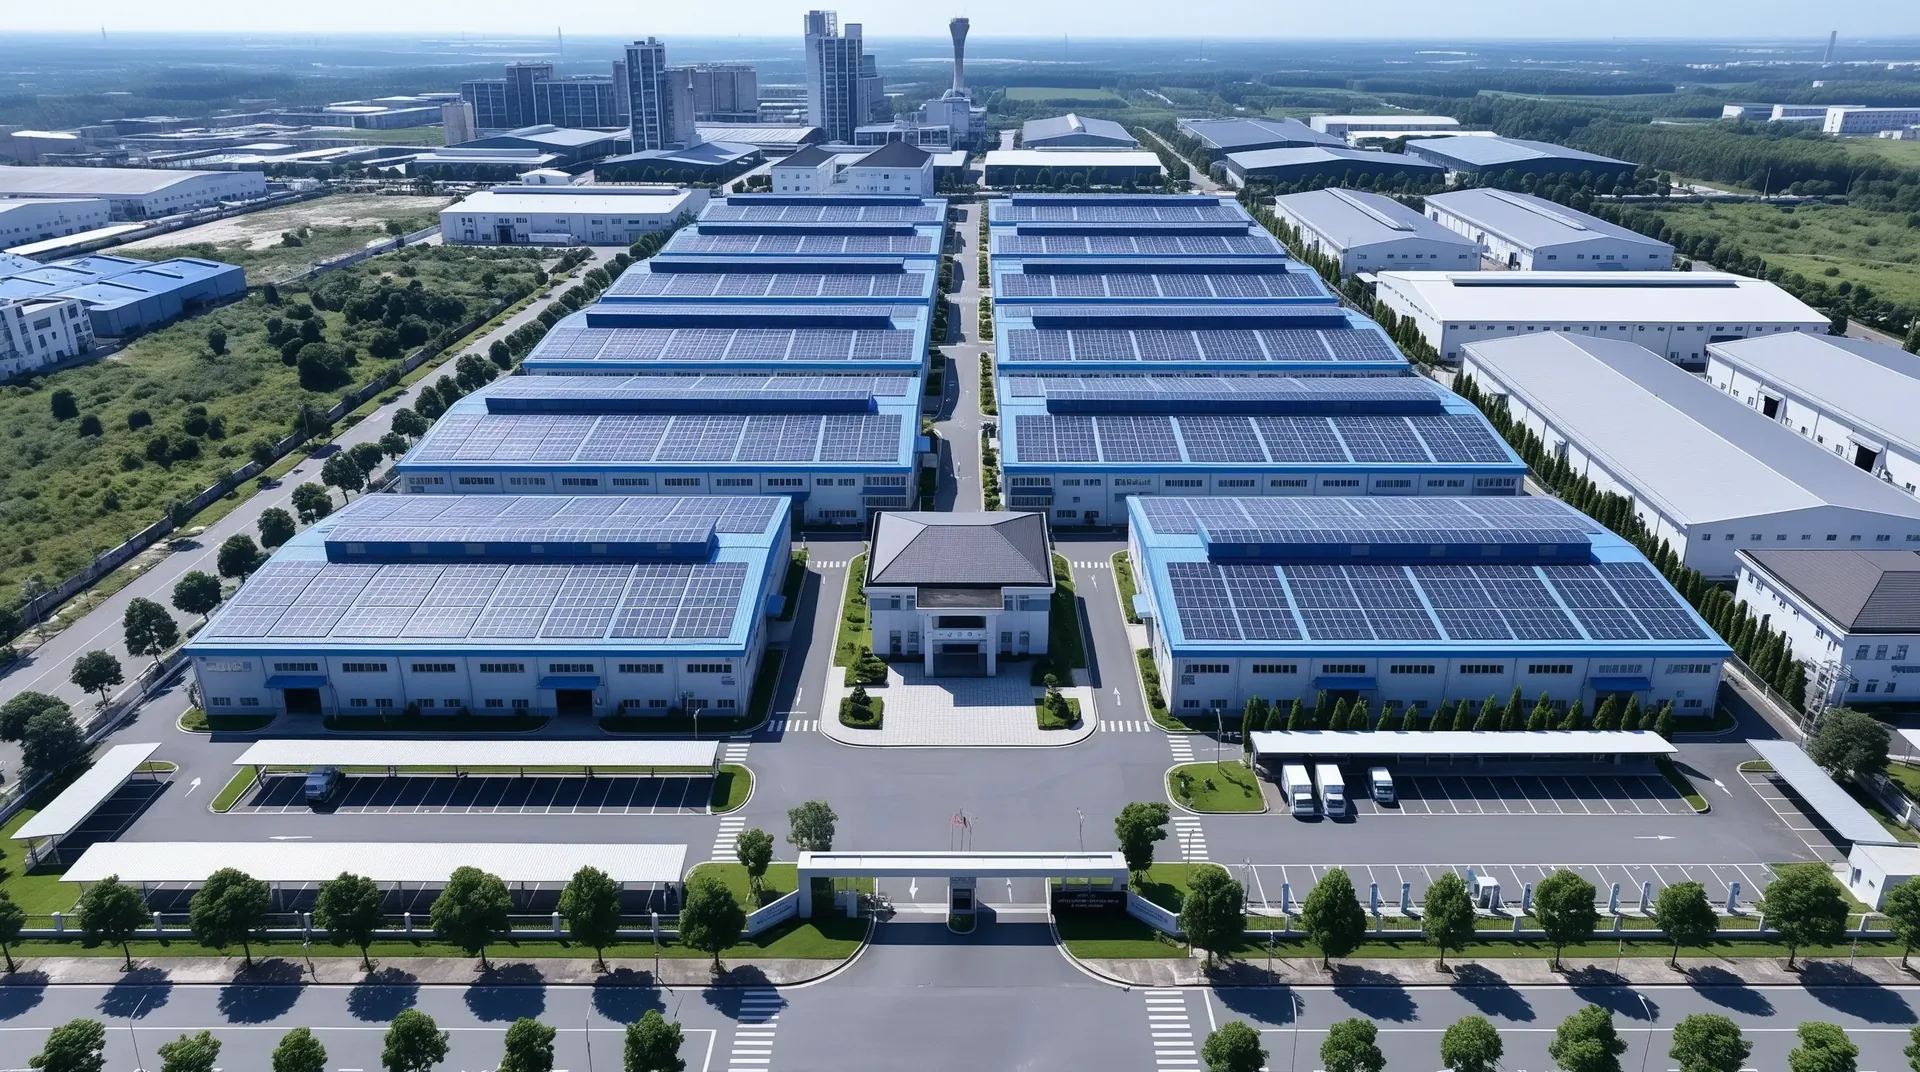
Proven Track Record
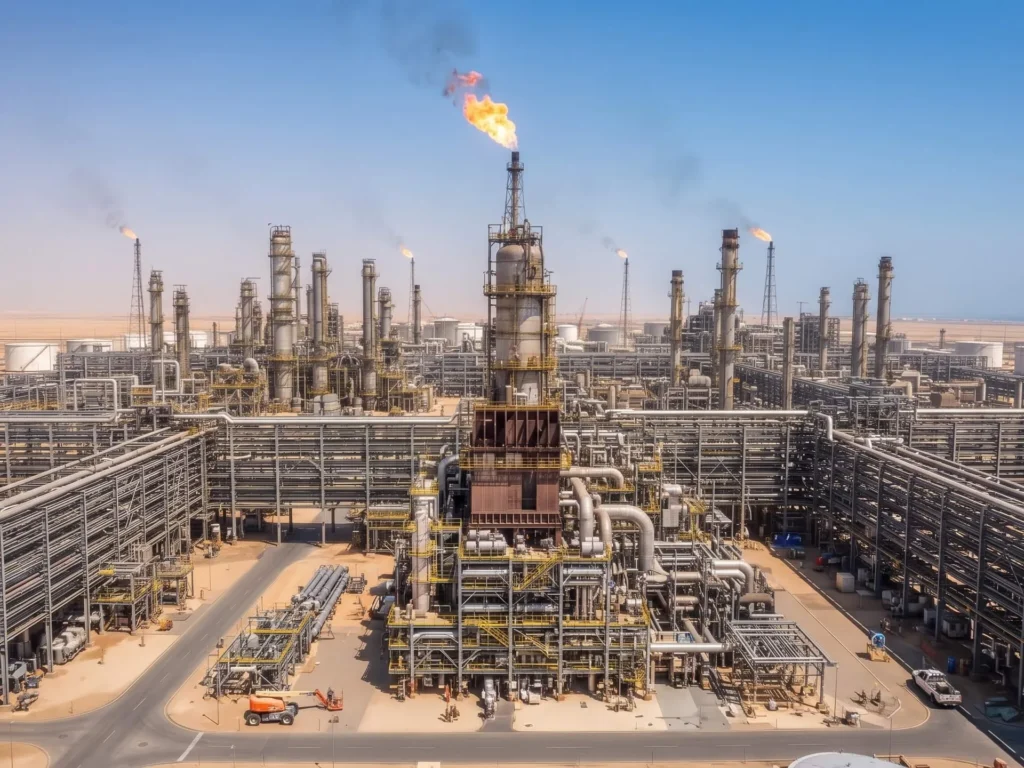
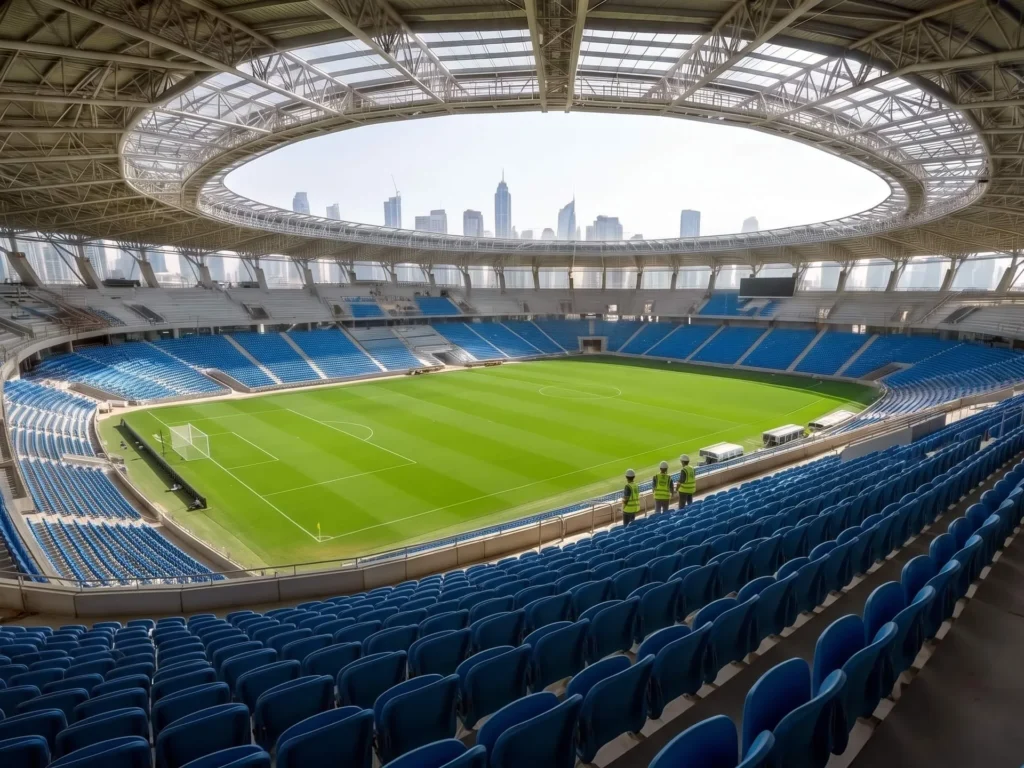
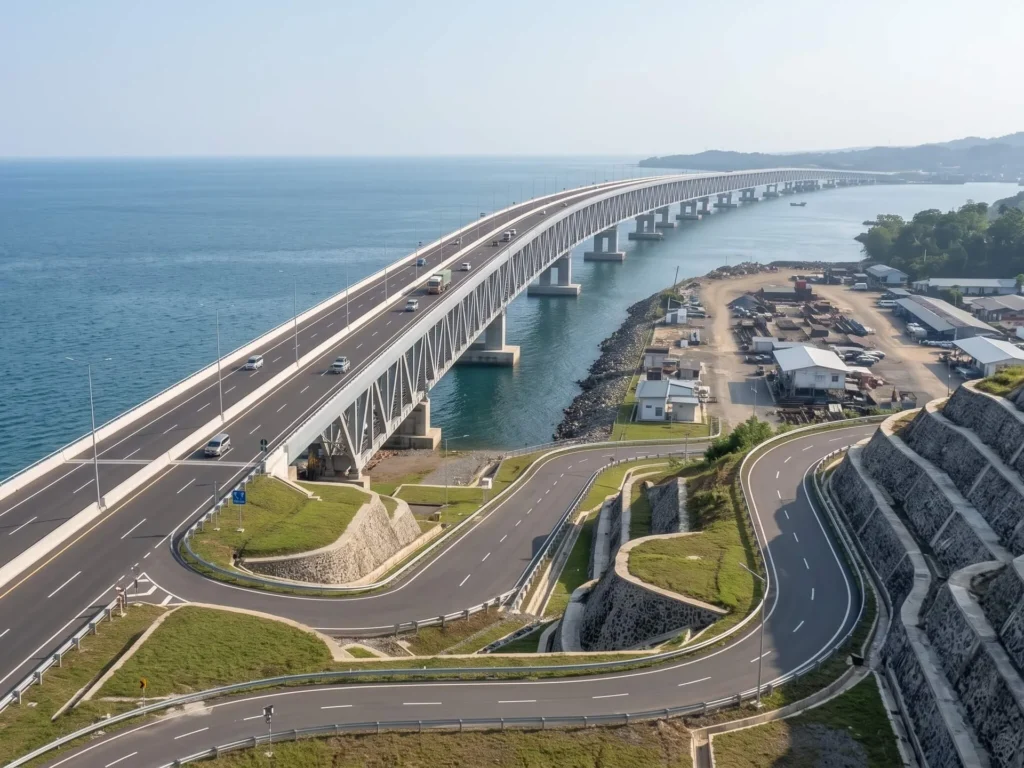
Discover how SynJect engineer certainty and eliminate on-site risks across the world's most demanding infrastructure projects.