Closed Environmentally Controlled Poultry House

Engineered Biosecurity

Modern high-density poultry production leaves no margin for structural or thermal failure. Backed by an 80,000 m² fabrication facility and 500,000-ton annual capacity, we manufacture precision-sealed PEB broiler and multi-tier layer houses engineered to hold 50 Pa negative pressure, resist severe ammonia corrosion, and safely carry automated feeding and climate systems.

Why Traditional Materials Fail in Modern Poultry Farming

In tunnel-ventilated poultry houses the structure directly dictates feed conversion ratio, flock mortality and HVAC electricity consumption. Replacing masonry, timber and angle-iron trusses with a solid-web PEB steel system removes four operational hazards.

Cross-section diagram of a closed poultry house showing laminar airflow entering through sidewall inlets, passing tiered cage equipment under negative pressure and exiting through end-wall exhaust fans
THE CHALLENGE

Masonry cracks and timber warps under humidity, so static pressure drops below 15 Pa. The result is dead air zones, heat-stress mortality and a 30% spike in exhaust fan electricity bills.

SynJect ENGINEERED SOLUTION

Millimetre-sealed envelope: ±1.0 mm CNC framing with tongue-and-groove PIR/PU sandwich panels and butyl-sealed joints holds 35–50 Pa negative static pressure, giving uniform wind-chill velocity across the whole flock.

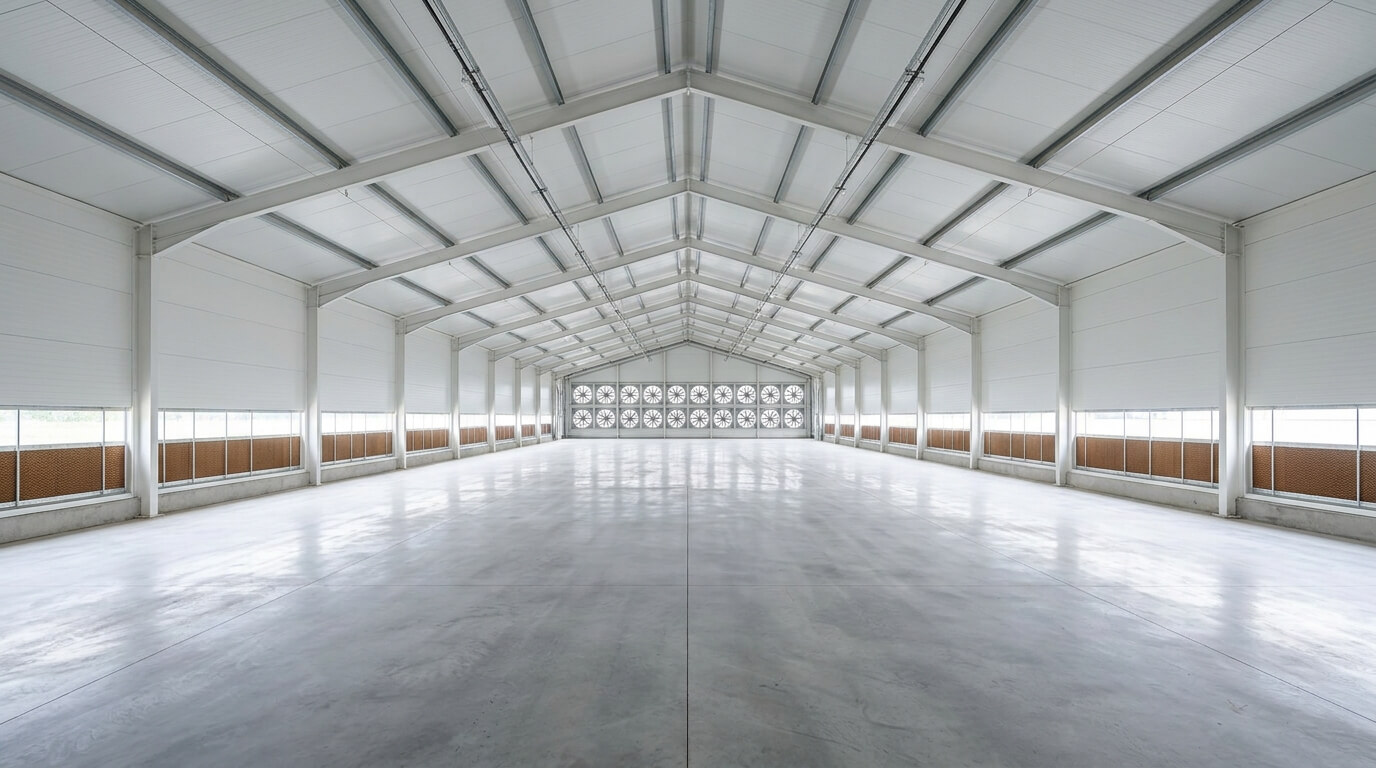
Poultry house interior with flush white wall panels, smooth under-purlin ceiling and evaporative cooling pads along the sidewalls
THE CHALLENGE

Porous timber and exposed truss chords trap infective dust, feathers, Salmonella, avian influenza and darkling beetles. Exposed insulation is destroyed by rodents and high-pressure washdown.

SynJect ENGINEERED SOLUTION

Zero-harbourage smooth interior: solid-web tapered H-beams with a flush under-purlin ceiling or double-sided FRP/Plastisol lining, able to take 150-bar hot-water and acid/alkali disinfection with no pathogen retention between flocks.

Close-up of a hot-dip galvanized steel connection showing zinc spangle texture, stainless bolts and bonded sealing washers
THE CHALLENGE

Litter emits concentrated ammonia above 20 ppm plus hydrogen sulphide, and evaporative cooling pushes relative humidity past 80%. Painted steel trusses rust through at the welds within three to five years.

SynJect ENGINEERED SOLUTION

C5-A agricultural corrosion matrix: primary frames shot-blasted to ISO 8501-1 Sa 2.5 and hot-dip galvanized to ASTM A123 (≥ 85 μm / 600 g/m²). Secondary purlins use self-healing ZAM ZM275 steel with SS304 or Dacromet fasteners.

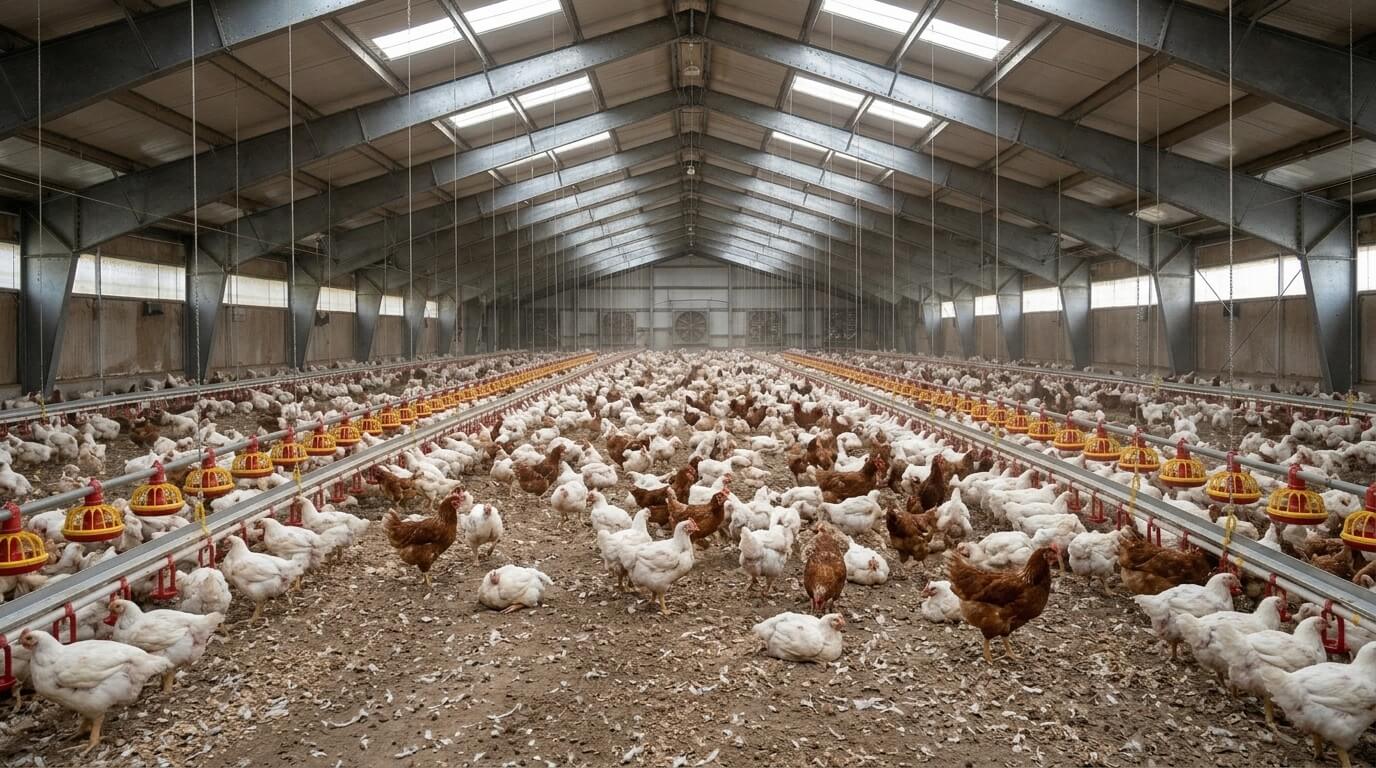
steel building for Poultry house
THE CHALLENGE

Interior columns obstruct pan feeders and skid-steer cleanout, and uncalculated trusses deflect or collapse when jammed auger lines load the roof.

SynJect ENGINEERED SOLUTION

12–32 m column-free spans with 0.25–0.60 kN/m² of equipment collateral load built into the Tekla LOD 400 calculation, including pre-punched bottom-flange suspension tabs for feeding and climate equipment.

THE CHALLENGE
SynJect ENGINEERED SOLUTION

Technical Specification Matrix

Every structure is calculated to local wind, snow and seismic codes (ASCE 7 / ASABE EP288 / Eurocode 3) and manufactured under CE EN 1090-1 EXC3 quality management.

Engineering parameter Floor-rearing broiler / breeder house Multi-tier caged layer / pullet house
Clear span width (column-free) 12.0 – 20.0 m (40–65 ft) 15.0 – 32.0 m (50–105 ft), 4–8 rows of H-cages
Eave height 2.6 – 3.5 m (high tunnel air velocity) 5.0 – 10.5 m (4–12 cage tiers plus manure pit)
Building length 80 – 150 m (matched to static pressure drop) 90 – 160 m (expansion joints over 120 m)
Roof pitch 1:10 – 1:12 (8–10%), flush interior ceiling 1:10 – 1:8 (10–12.5%)
Design collateral load (roof) 0.25 – 0.35 kN/m² (feeders, drinkers, brooders, inlets) 0.35 – 0.60 kN/m² (ceiling inlets, lighting, catwalk)
Negative pressure resistance Continuous 50 – 60 Pa inward suction Continuous 50 – 60 Pa inward suction
Primary steel grade & coating Q355B/D tapered H-beam, HDG ≥ 85 μm (ASTM A123) Q355B/D heavy H-beam, HDG ≥ 85 μm or C5 epoxy system
Secondary purlins / girts S350GD cold-formed ZAM (ZM275) S350GD cold-formed ZAM (ZM275)
Roof & wall insulation 75 – 120 mm PIR/PU sandwich panel (R ≥ 3.5–5.0) 75 – 150 mm PIR/PU or high-density rockwool
Pre-framed equipment openings Gable 50″/54″ cone fans, tunnel doors, sidewall cooling pads Multi-level exhaust fan banks, cooling rooms, egg conveyor tunnels

NoteVentilation, feeding and climate equipment layouts shall be coordinated with the integrator prior to fabrication.

How Your Project Is Built

Agricultural projects often mean ten to fifty identical houses in a remote region. The three stages below exist to protect capex and schedule at that scale.

PHASE 01 / LOGISTICS

3D Container Nesting & Packing

Rafters are segmented and ZAM purlins and PIR panels are nested using 3D volumetric simulation, lifting 40HQ loading efficiency from around 60% to over 85% and cutting ocean freight per bird housed.

PHASE 02 / ERECTION

Pre-Punched, Zero-Welding Assembly

Every H-beam, wind column and fan-framing channel is CNC-drilled and hard-stamped with Tekla part numbers. Local crews bolt the structure together with HSFG bolts, cutting commissioning time by up to 40%.

PHASE 03 / HANDOVER

Pressure Test & Documentation

Before handover the envelope is checked for airtightness against the design negative pressure, and the structural file is issued for the integrator and the local authority.

Qualification Certificate

Your projects are protected by world-class standards. From CE (EN 1090) to ISO 9001, our qualifications are not just paper—they are the rigorous daily reality on our shop floor.

AISCCEOTCInternational Welder
ISO 9001 Quality Management System

Recommended Product Systems

Frames, purlins and envelope systems for poultry houses, from one fabrication source.

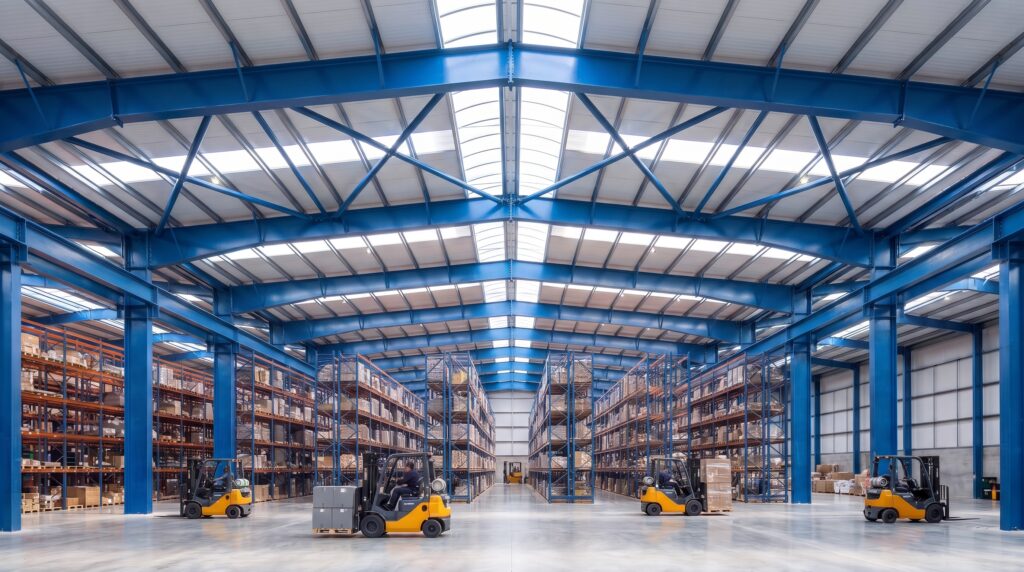
Interior of a multi-span steel portal frame warehouse with blue columns, pallet racking aisles, forklift trucks and roof cross bracing

SynJect manufactures precision-engineered Portal Frames designed to maximize column-free interior space while minimizing material and shipping costs. Operating an 80,000 m² facility, we deliver robust structural frameworks tailored for global logistics parks and heavy manufacturing plants.

Frequently Asked Questions

How do you prevent roof collapse when automated feed augers jam or overload?

Generic warehouse suppliers calculate only dead and live roof loads. We engineer a dedicated 0.25 to 0.60 kN/m² collateral load into the primary rigid frames and purlins, with deflection limits of L/240 to L/360, so the roof never sags or breaks the seal at sidewall ventilation inlets.

For tunnel-ventilated houses with evaporative cooling pads and high litter humidity, we recommend full hot-dip galvanizing (≥ 85 μm) for primary frames and ZAM ZM275 for secondary purlins. Zinc bonds metallurgically to the steel, giving 25–30+ years of maintenance-free protection, whereas paint blisters and rusts at connection joints within a few years.

Yes. Share the equipment layout from your integrator and our Tekla LOD 400 detailers model every exhaust fan bank, evaporative cooling pad opening, tunnel door and sidewall inlet into the secondary framing. All sub-frames arrive pre-cut and ready to bolt.

Get Your 24-Hour BOQ and Cost Plan

See how much steel tonnage and ocean freight you can save before fabrication begins

8–15%

Steel Weight Savings

1:1 Tekla 3D modeling optimizes beam-column ratios to eliminate redundant material costs.

0.0mm

Zero-Clash Code Verification

Checked against EN 1090 and local wind/seismic loads.

100%

Engineer-to-Engineer Review

Verified by our lead engineers—Zero pushy sales calls, Just actionable data and factory price.

CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001

Engineering & Inquiry Desk

Lead Engineers Online

Drawings
Drawings

🔒 100% Private and Secure, No Spam