12,000-Ton Petrochemical Pipe Rack Modules
Fabricated in Map Ta Phut. C5-M coating, shop assembly. Completed 3 Weeks Ahead; zero hot-work permits in live zones.
Project Facts
The commercial and technical facts a contractor checks before requesting drawings.
| Industry | Mega Refinery Revamp & Petrochemical Complex |
|---|---|
| Location | Map Ta Phut, Rayong Province, Thailand (Gulf of Thailand) |
| Design & Execution | AISC 360, AWS D1.1, ASTM A123, ISO 12944 (C5-M) |
| Service Environment | Tropical monsoon, >80% RH, heavy salt spray & chemical vapors |
| Delivery Result | Completed 3 Weeks Ahead; zero hot-work permits in live zones |
| Total Volume | Over 12,000 Metric Tons of heavy structural steel |
| Our Scope | Fabrication, C5-M coating, shop assembly and delivery |
Project Overview
How the structure was engineered, fabricated and delivered in Map Ta Phut.
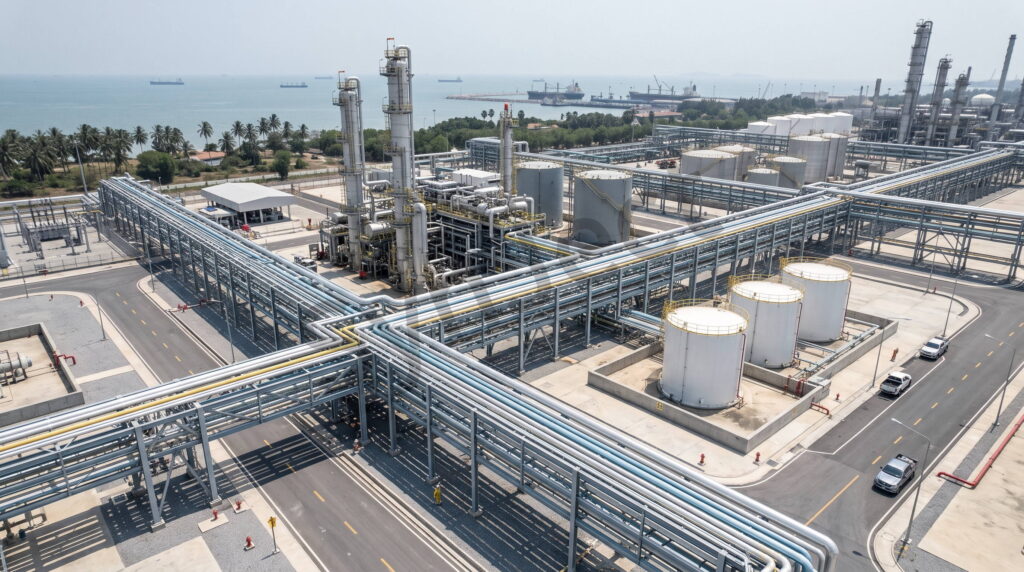
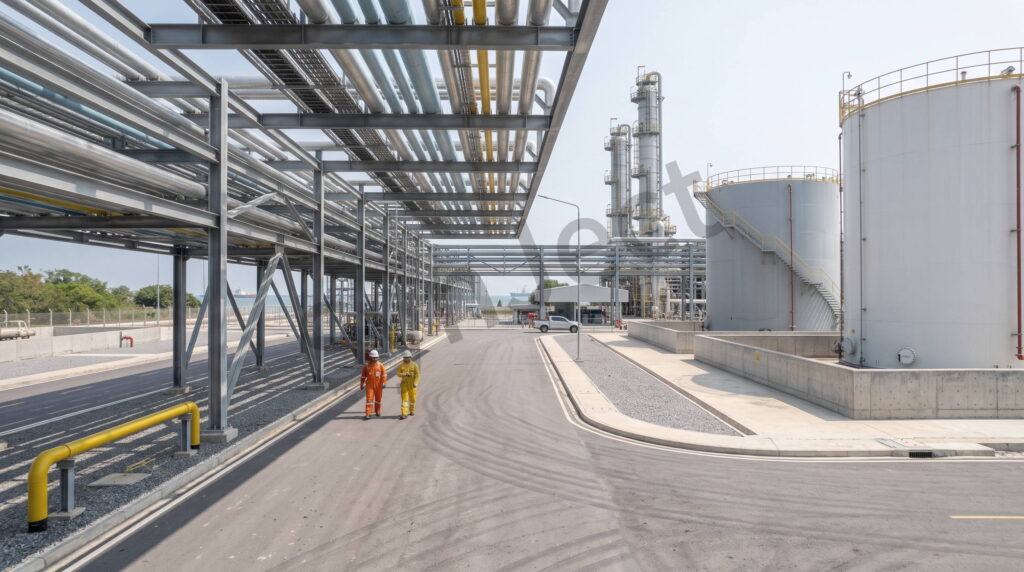
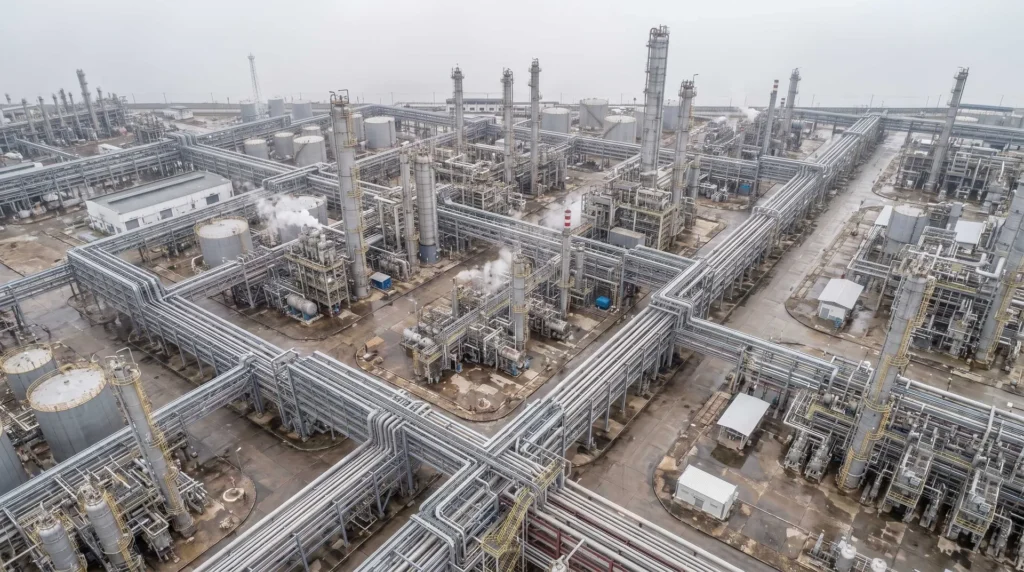
Located in the Map Ta Phut Industrial Port zone along the Gulf of Thailand, this mega-scale refining and petrochemical revamp demanded the fabrication of over 12,000 tons of heavy multi-tier process pipe racks weaving through active chemical units.
In this tropical coastal environment, continuous high humidity (averaging >80%), seasonal monsoon downpours, and intense marine chloride exposure pose severe long-term corrosion hazards.
Moreover, with high-pressure hydrocarbon, steam, and chemical lines crisscrossing the complex, any deflection in the steel trestles or alignment error on pipe supports can trigger catastrophic pipeline fatigue stresses.
The project operated under uncompromising QA/QC mandates governed by AISC 360, AWS D1.1, ASME B31.3, and ASTM A123.
Four Decisions That Made It Work
Sub-Millimeter Clash-Free Fabrication
Integrated Tekla BIM with multi-tier piping stress models, ensuring tens of thousands of bolt connections aligned seamlessly without field reaming or torch
Duplex Coastal Tropical Anti-Corrosion
Heavy-duty hot-dip galvanizing exceeding ASTM A123 coupled with a UV-resistant polyurethane topcoat (ISO 12944 C5-M compliant) ensures a 30+ year service l
Zero-Hot-Work Erection in Hazardous Zones
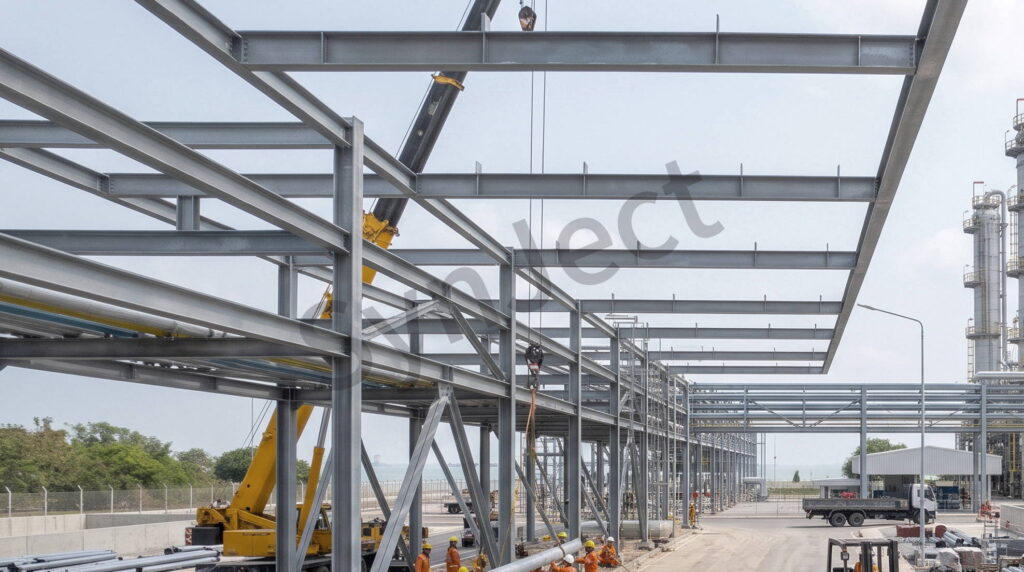
Fully bolt-together connection designs eliminated on-site flame cutting and welding inside volatile refinery operating zones, substantially decreasing proj
Smart Tagging & Lean Site Logistics
Applied weatherproof QR coding matched to structural erection phases, slashing on-site unloading, sorting, and staging time by 40%.
The Project, As Built
Completed works, structural details and the delivery team on site.


Client Testimonial
Feedback recorded from the client after handover.
Erecting pipe racks in live petrochemical zones leaves zero room for errors. Shijie nailed it—100% bolt-aligned, zero field modifications, 3 weeks ahead!
Frequently Asked Questions
Answers engineers ask before committing to a scope like this.
What did SynJect fabricate for this Map Ta Phut refinery revamp?
More than 12,000 tonnes of heavy multi-tier steel trestles and cross-braced portals, threaded through operating chemical units to carry high-pressure hydrocarbon, steam and chemical lines. Design followed AISC 360 and AWS D1.1, with corrosion protection to ISO 12944 C5-M.
Humidity above 80% plus constant chloride spray will destroy a paint system. What was used?
Heavy-duty hot-dip galvanising exceeding ASTM A123, with all edges radiused before dipping, followed by a UV-resistant polyurethane topcoat. Galvanising protects cut edges and bolt threads that a paint-only system leaves exposed in a coastal monsoon climate.
High-pressure lines push cyclic horizontal loads into the racks. How is that absorbed?
Slotted friction-grip slip joints and gusset-stiffened moment frames dissipate the thermal thrust instead of feeding it into the connections. The rack was detailed against the piping stress model, so expansion moves where it is designed to move.
Can racks be erected inside a live, hazardous process unit?
Yes, because the design is fully bolt-together. No on-site flame cutting and no welding inside the volatile zones, so no hot-work permit and no shutdown window was consumed by steel erection.
Staging space inside an operating plant is almost zero. How was material handled?
Every member was packaged just-in-time in erection sequence and marked with weatherproof QR codes matched to the structural phases. Cranage lifts straight from the delivery truck, which cut unloading, sorting and double handling on a site that had no laydown area.
Get Your 24-Hour BOQ and Cost Plan
See how much steel tonnage and ocean freight you can save before fabrication begins
Steel Weight Savings
1:1 Tekla 3D modeling optimizes beam-column ratios to eliminate redundant material costs.
Zero-Clash Code Verification
Checked against EN 1090 and local wind/seismic loads.
Engineer-to-Engineer Review
Verified by our lead engineers—Zero pushy sales calls, Just actionable data and factory price.
CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001
Lead Engineers Online
🔒 100% Private and Secure, No Spam