Resources Steel Facilities · United Arab Emirates (UAE)

±1.0 mm Modular Process Skids

Fabricated in Abu Dhabi. Saved 45 Days of desert site installation time.

85 tSteel Tonnage
18 mModule Size
+52 °CDesign Temperature
45 DaysDelivery Schedule

Project Facts

The commercial and technical facts a contractor checks before requesting drawings.

Project facts and specifications
IndustryOnshore Modular Gas Processing & Separation
LocationAbu Dhabi, United Arab Emirates (UAE)
Project ScaleUp to 18m (L) × 6.5m (W) × 5.2m (H); up to 85 Tons/unit
Design & ExecutionADNOC Specs, ASME Sec. VIII Div.1, ASME B31.3, AWS D1.1
Service Environment+52°C extreme desert heat, fine silica sand abrasion, UV
Delivery ResultSaved 45 Days of desert site installation time
Our ScopeHeavy Skid Baseframes, Vessels & Pre-assembled Piping

Project Overview

How the structure was engineered, fabricated and delivered in Abu Dhabi.

Located in the desert hinterland of Abu Dhabi (Habshan/Ruwais energy corridor), this critical upstream gas processing facility demanded rapid expansion under unforgiving conditions.

In the Middle Eastern desert, remote on-site fabrication faces extreme ambient heat exceeding +52°C, choking sandstorms, and exorbitant field labor and logistics costs.

To compress the construction schedule and ensure absolute plant reliability, the EPC client adopted a comprehensive "Plug-and-Play" modularization strategy, requiring dozens of heavy process skids integrating high-pressure piping manifolds, ASME Section VIII separation vessels, shell-and-tube heat exchangers, and high-rigidity structural steel baseframes.

The project had to strictly adhere to ADNOC specifications, ASME B31.3, AWS D1.1, and ISO 12944 C5-I/C5-M marine-desert corrosion standards.
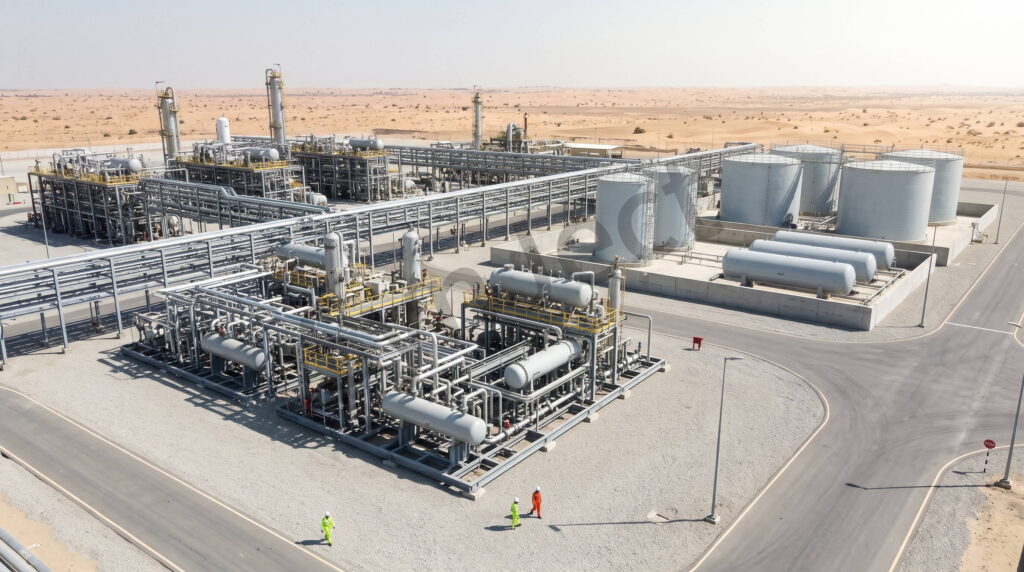
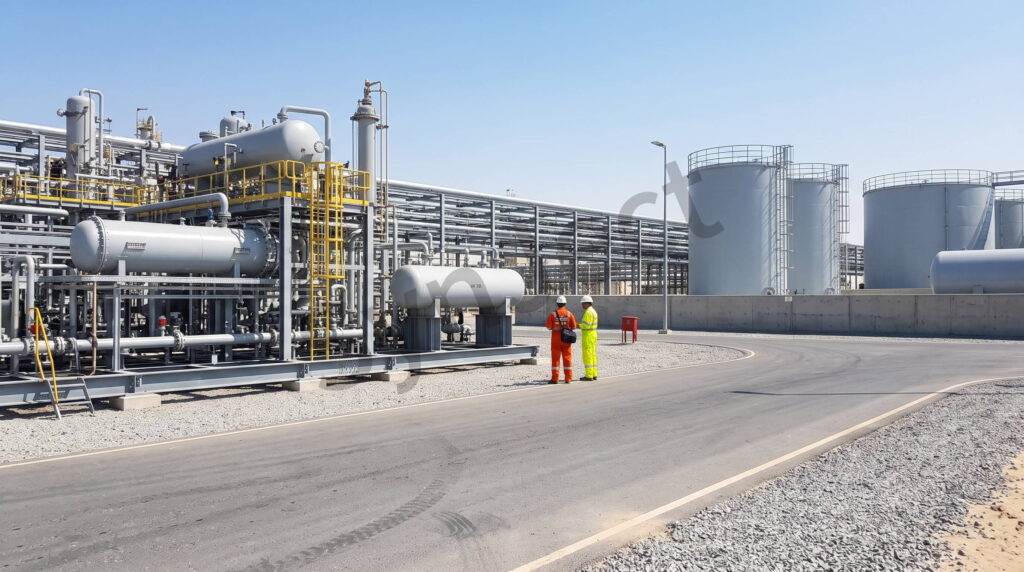
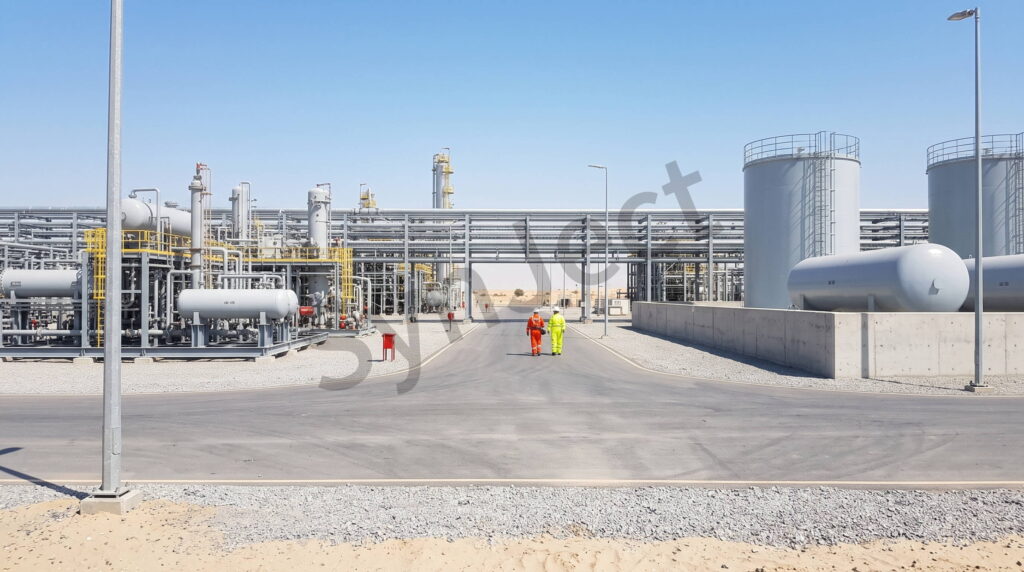
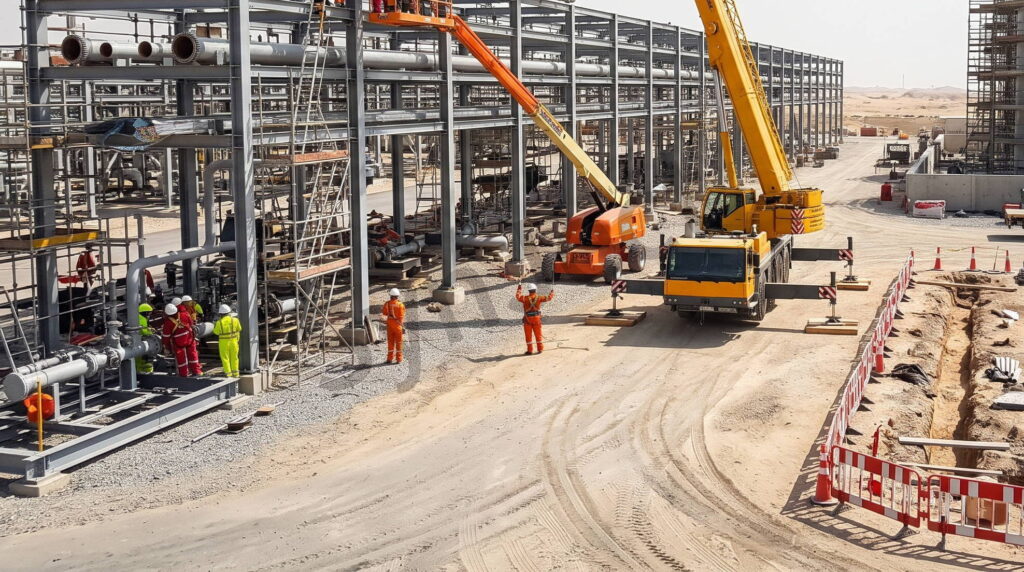
High-Precision Modular Process Skids & Heavy Skid Structural Frames for Mega Gas Processing Facility in Abu Dhabi, UAE - completed steel structure photograph 1, delivered

Four Decisions That Made It Work

01

Plug-and-Play Modular Integration

Fully integrated mechanical, piping, and vessel structures in-shop, enabling rapid flanged hookups and reducing on-site tie-in connections by over 80%.

02

Sub-Millimeter Baseframe Rigidity

Heavy H-beam and box girder skid base engineered to withstand multi-point lifting and desert transport twists without transferring deflection to sensitive

03

100% First-Pass NDT Dual Testing

Robotic submerged arc welding (SAW) and qualified low-hydrogen procedures ensured complete joint penetration (CJP) weldments were 100% free of porosity or

04

Desert-Resistant Heavy-Duty Coating

Sa 2.5 blast profile coupled with a three-coat inorganic zinc-rich and polyurethane system resilient against +50°C solar radiation and abrasive silica dust

Client Testimonial

Feedback recorded from the client after handover.

Fabrication and installation team at project handover
“

In Abu Dhabi’s brutal desert, Shijie’s modular skids delivered surgical precision—zero field modifications, saving 45 days of high-risk site work!

Mansoor Al-H.Upstream Project Delivery Manager (Abu Dhabi)
85 t18 m+52 °C

Frequently Asked Questions

Answers engineers ask before committing to a scope like this.

What exactly are these skids and how large are they?

They are heavy plug-and-play process skids for an onshore gas processing facility in the Habshan-Ruwais corridor: baseframes up to 18 m long, 6.5 m wide and 5.2 m high, weighing up to 85 tonnes each, carrying high-pressure piping manifolds and ASME Section VIII Div.1 vessels on H-beam and box-girder baseframes.

The baseframe is modelled in 3D FEA for multi-point lifting and desert road transport, then fitted with temporary stiffening cradles and transport saddles for the journey. Rigidity is verified before shipment, so the piping interfaces arrive square and bolt up without field rework.

Every skid is modelled in full 3D CAD and Tekla against the pipe stress model, with clash detection run before fabrication. Critical interfaces are pre-checked with a shop laser tracker, so flanges and supports land within tolerance instead of being cut and re-welded on site.

Robotic submerged arc welding with qualified low-hydrogen procedures to AWS D1.1, with complete joint penetration verified by first-pass NDT. Hydro-testing is also completed in the shop, so the skid arrives tested rather than waiting for a site test package.

Yes. Steel is blast cleaned to Sa 2.5 with a 50-75 micron profile, then coated with an inorganic zinc-rich primer and polyurethane topcoat to ISO 12944 C5-M/C5-I, giving both abrasion resistance and UV stability in desert service.

Get Your 24-Hour BOQ and Cost Plan

See how much steel tonnage and ocean freight you can save before fabrication begins

8–15%

Steel Weight Savings

1:1 Tekla 3D modeling optimizes beam-column ratios to eliminate redundant material costs.

0.0mm

Zero-Clash Code Verification

Checked against EN 1090 and local wind/seismic loads.

100%

Engineer-to-Engineer Review

Verified by our lead engineers—Zero pushy sales calls, Just actionable data and factory price.

CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001

Engineering & Inquiry Desk

Lead Engineers Online

Drawings
Drawings

🔒 100% Private and Secure, No Spam