
Home / Solutions / Industrial Steel Buildings / Slaughter & Meat Processing Workshop

PEB Steel Building for Slaughterhouse & Meat Processing Plant Solutions

Heavy-Duty Manufacturing.

We deliver more than just a building shell; we provide a Sanitary Design industrial foundation that flawlessly supports “thousand-ton overhead carcass logistics,” defies daily 80°C caustic washdowns, and thoroughly eradicates Listeria breeding grounds.

Core Pain Points & Solutions

Engineering Risk Control Driven by Slaughtering Processes and Operating Conditions

From hygienic zoning and wet-area drainage to equipment loading and cold-chain enclosure performance, we address the critical risks arising from high humidity, intensive wash-down, continuous production and stringent hygiene requirements—before they become operational problems.

THE CHALLENGE

Chillers and boning lines rely on “top-down” suspended operations. Hundreds of carcasses sliding on tracks create dynamic swaying. Standard light-steel roofs visibly deflect under these extreme point loads, deforming twin-tracks. A jammed trolley or fallen heavy rail instantly halts the slaughter line, losing capacity and endangering lives.

SynJect ENGINEERED SOLUTION

We reject generic plant designs. Our engineers extract precise rail load data directly from your equipment suppliers (e.g., Marel, Jarvis) to design high-rigidity Lattice Girders or heavy space trusses, providing 1.5-3.5 kN/m² of suspended loads. All suspension hangers are 100% precision-located and fully welded before shipping, absorbing all swaying forces to ensure zero rail deformation over 20 years of full-load operation.

THE CHALLENGE

Slaughterhouses are literal “corrosion hells.” Bleeding zones are soaked daily in salty blood; night sanitation crews use harsh caustic soda, hypochlorite, and 80°C water for high-pressure washdowns. If standard steel columns sit directly on the floor, the bases blister and flake within 6 months. Rust falling into meat means astronomical claims, and rotted bases cause building settlement.

SynJect ENGINEERED SOLUTION

We arm anti-corrosion to the teeth. In high-frequency washdown zones, steel columns never directly touch the floor. We elevate the concrete pedestals by 300-500mm and seamlessly clad them with welded 304/316L Stainless Steel Curbs. This completely cuts off the corrosion source, allowing workers to blast the column bases with high-pressure washers fearlessly, extending plant lifespan beyond 25 years.

THE CHALLENGE

Traditional H-beams have wide horizontal flanges. During splitting and deboning, meat aerosols and bone dust splatter and accumulate on these unreachable high-altitude blind spots, rotting and molding. When food safety inspectors take environmental swabs there, Listeria or Salmonella will absolutely exceed limits, causing devastating shutdowns and brand crises.

SynJect ENGINEERED SOLUTION

Strictly adhering to AMI Sanitary Design guidelines. In exposed meat zones, we replace all main and secondary structures with Circular Hollow Sections (CHS) or diamond-oriented square tubes. This thoroughly eradicates dust-trapping horizontal surfaces; all tube ends are mandatorily fully seal-welded to prevent condensation and blood from seeping inside; all welds are ground flush. Bacteria lose their hiding spots, making audits a breeze.

THE CHALLENGE

Steaming hot, freshly slaughtered carcasses are pushed into 0-4°C chillers. The extreme temperature shock generates massive moisture. If insulation between steel hangers and the ceiling is poor, creating “thermal bridges,” the ceiling sweats profusely. A single drop of dirty water on the raw meat below condemns the entire high-value batch for destruction.

SynJect ENGINEERED SOLUTION

We mandatorily insert high-strength nylon Thermal Breaks at suspension nodes between the load-bearing steel and cold room ceiling, thoroughly severing external heat conduction through the metal. Combined with 150-200mm PIR food-grade panels, we create an absolutely moisture-proof “Box-in-Box.” Ceilings remain eternally dry and drip-free, safeguarding food safety while slashing refrigeration power bills.

THE CHALLENGE

Slaughterhouses have incredibly strict floor drainage requirements (mandatory 1-2% slopes). Builders unfamiliar with slaughter processes often place steel columns exactly on the path of main drainage trenches or in floor valleys. This causes massive amounts of fat residue and blood to bypass traps, pooling and rotting around column bases, making cleaning a nightmare.

SynJect ENGINEERED SOLUTION

During pre-construction detailing, we mandate importing your “Workshop Drainage Network & Floor Slope Plan” into our Tekla steel model. Structural engineers proactively adjust every column’s span and footprint to strictly avoid main stainless steel sewer trenches and catch basins. We ensure columns always stand on the floor’s “high ground,” allowing washdown water and gravity to swiftly carry blood into grease interceptors.

Technical Specifications for Slaughterhouse Facilities

These specifications are not generic standard values. They are engineered according to slaughtering processes, production capacity, equipment loads, hygienic zoning, local climate and applicable building codes. The ranges below are typical design references; final values are confirmed through project calculations, equipment data and local regulations.

Technical Parameter Typical Range / Requirement
Customization Available
Clear Span 18–40 m, process-dependent
Eave Height 6–12 m, equipment-dependent
Structural Grid Approx. 6–9 m, process-optimized
Overhead Rail Elevation Process-specific
Rail Load Calculated from carcass, hanger and dynamic effects
Equipment Point Load Based on supplier data
Wet-Area Floor Slope Typically 1–2%, subject to drainage design
Drainage Hydraulic and solids-load based
Hygienic Flooring PU concrete, polyurethane mortar or resin system
Hygienic Wall System Insulated hygienic panels
Cold-Room Insulation value calculated by room temperature and climate
Condensation Control Surface temperature above dew point with safety margin
Corrosion Protection ISO 12944 C3–C5, environment-dependent
Ventilation Design Process and load-based calculation
Hygienic Zoning Dirty–Transition–Clean–Chilled
Future Expansion Based on future capacity planning

NoteAll critical parameters should ultimately be project-engineered according to the slaughtering process, equipment data, production capacity, local climate and applicable building codes.

Construction Process Showcase

The objective of a slaughterhouse project is not simply to complete a steel building, but to accurately integrate slaughtering processes, hygienic zoning, equipment systems, structural systems, drainage, building envelope, refrigeration and utilities at every stage.

PHASE 01 / PRE-CONSTRUCTION

Resolve Risks During Design

Preemptively resolving clashes among suspended logistics and sewer networks via BIM, eliminating on-site errors.

PHASE 02 / CONSTRUCTION

Dust-Free Dry Assembly & 3D Heavy Anti-Corrosion

Rapid all-bolted assembly paired with stainless steel column cladding, racing for the optimal schedule in a dust-free environment.

PHASE 03 / COMPLETION

Full-Load Simulation Testing & Audit-Ready Delivery

Move Beyond Construction Completion to Production-Readiness Verification, Ensuring the Facility Is Prepared for Equipment Installation, Trial Operation and Full Commissioning.

Qualification Certificate

Your projects are protected by world-class standards. From CE (EN 1090) to ISO 9001, our qualifications are not just paper—they are the rigorous daily reality on our shop floor.


AISCCEOTCInternational Welder
ISO 9001 Quality Management System
Recommended Product Systems

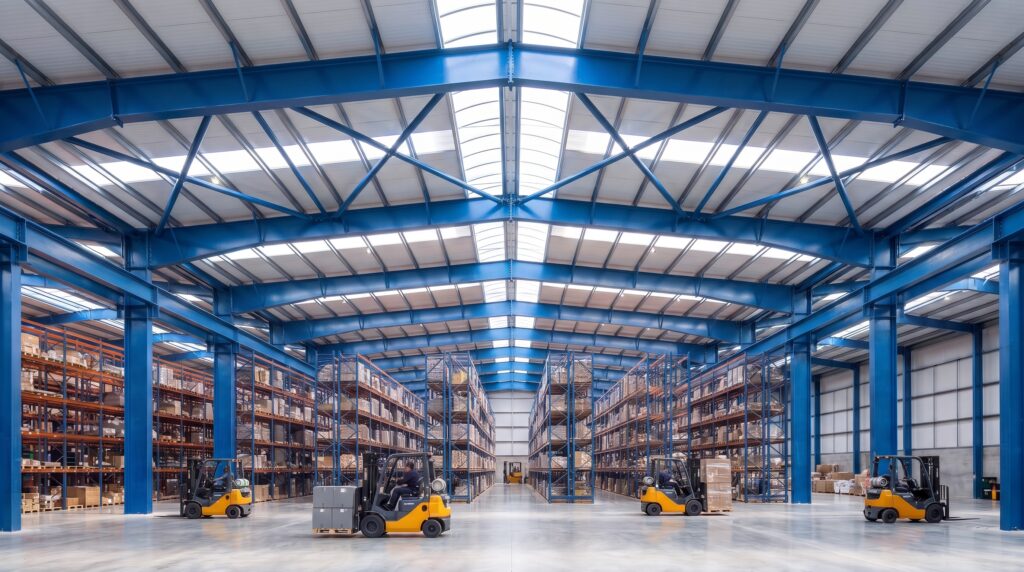
Interior of a multi-span steel portal frame warehouse with blue columns, pallet racking aisles, forklift trucks and roof cross bracing

SynJect manufactures precision-engineered Portal Frames designed to maximize column-free interior space while minimizing material and shipping costs. Operating an 80,000 m² facility, we deliver robust structural frameworks tailored for global logistics parks and heavy manufacturing plants.

Steel Truss

SynJect Steel Truss systems deliver unparalleled heavy load-bearing capacity and clear-span flexibility.

Completed steel structure cladding system project delivered by SynJect

SynJect Envelope & Cladding Systems seal your structures with superior thermal performance and weatherproofing.

Frequently Asked Questions

What special requirements should be considered when designing steel structures for a slaughterhouse?

A slaughterhouse must meet more than standard industrial building requirements. Design considerations include high humidity, frequent washdown, cleaning and disinfection procedures, processing equipment layouts, drainage gradients, and personnel and material flows. The steel structure should be coordinated with the processing layout, equipment loads, building envelope, and hygiene requirements to avoid conflicts with production and cleaning operations.

Durability can be improved through an appropriate corrosion-protection system and carefully detailed connections, but standard paint alone may not address every corrosion risk. Before design, the project team should identify humidity levels, washdown frequency, cleaning chemicals, chloride exposure, and condensation risks. The coating system and detailing should then be selected accordingly, with particular attention to water traps, crevices, cut edges, and hard-to-maintain areas. The final specification should reflect actual site conditions, applicable standards, and maintenance requirements.

Production-line layouts, equipment dimensions, conveyor paths, maintenance clearances, and personnel routes should be reviewed alongside the structural design. For overhead conveyor systems, lifting equipment, and other structure-supported machinery, the loads, suspension points, dynamic effects, and installation requirements must be defined in advance. Coordinating the column grid, beam positions, clear heights, and equipment interfaces helps reduce structural modifications during construction. Process design and specialist equipment performance remain the responsibility of the relevant suppliers and design teams.

The structure can be designed to support these systems when the loading information is clearly defined and verified by structural calculations. The client should provide equipment weights, operating loads, start-stop or impact effects, suspension-point locations, operating conditions, and maintenance loads as early as possible. Loads from overhead rails and concentrated suspension points must not simply be treated as uniformly distributed roof loads. Actual load paths, member capacities, connection details, and overall stability must be checked using confirmed data from the equipment supplier

.

Hygiene and cleaning requirements affect column bases, beam-to-column connections, wall interfaces, roof drainage, and equipment support locations. Details should minimize water traps and inaccessible cleaning areas, while coordinating with floor gradients, drains, wall cladding, and hygienic partitions. The steel structure itself does not replace food-hygiene design. Floor drainage, waterproofing, food-contact surfaces, and hygienic zoning must be developed with the architectural, process, and hygiene specialists.

Different areas often require different envelope solutions. Lairage, slaughtering and processing areas, cutting and packaging rooms, chilling rooms, and cold stores can have significantly different temperature, humidity, cleaning, and condensation conditions. Cladding and insulation should be selected according to target temperatures, thermal performance, airtightness, washdown resistance, vapor control, and fire requirements. The steel structure team should coordinate with the envelope and refrigeration specialists, paying particular attention to thermal bridges, condensation, and panel joints.

Before construction, the project team should finalize the main structural design, confirm equipment interfaces, approve fabrication drawings, and plan procurement of critical materials. Where conditions permit, off-site fabrication can proceed in parallel with foundation works. Marking, packing, and shipping members in erection sequence helps reduce on-site rework and waiting time. The actual schedule depends on approvals, foundation readiness, equipment-interface confirmation, transportation, lifting conditions, and local construction requirements; a fixed completion period should not be promised without project-specific information.

Structural design should follow the applicable building codes for the project location, considering basic wind pressure, seismic parameters, snow loads where applicable, occupancy loads, structural importance, and ground conditions. For international projects, the governing design codes, material standards, connection requirements, and approval-document formats should be established early. The engineering team can define the design basis once the project location, site information, building use, and relevant design inputs are available. Final compliance remains subject to local regulations and review by appropriately qualified professionals.

Long-term maintenance costs can be reduced by considering corrosion durability, inspection access, drainage, cleanability, and component replacement during design. The protection system should suit the actual exposure conditions, while details should avoid water traps and inaccessible concealed areas. A maintenance plan should cover coating inspections, localized repairs, and periodic condition assessments. Particular attention is needed at column bases, connections, cut edges, and envelope interfaces exposed to washdown water or cleaning chemicals. Maintenance intervals should be based on the protection system, site conditions, and inspection findings.

Buyers should verify that the manufacturer has suitable detailing and fabrication capabilities for the project scale and can provide material traceability, welding quality control, dimensional inspection, surface-treatment records, and member identification as required. They should also confirm the manufacturer's ability to coordinate interfaces with processing equipment suppliers, envelope contractors, and the erection team. The scope of supply, design responsibilities, inspection requirements, packing and shipping arrangements, and boundaries of on-site technical support should be clearly defined. Required certifications, third-party inspections, and documentation should be agreed upon during contract negotiations.

Get Your 24-Hour BOQ and Cost Plan

See how much steel tonnage and ocean freight you can save before fabrication begins

8–15%

Steel Weight Savings

1:1 Tekla 3D modeling optimizes beam-column ratios to eliminate redundant material costs.

0.0mm

Zero-Clash Code Verification

Checked against EN 1090 and local wind/seismic loads.

100%

Engineer-to-Engineer Review

Verified by our lead engineers—Zero pushy sales calls, Just actionable data and factory price.

CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001

Engineering & Inquiry Desk

Lead Engineers Online

Drawings
Drawings

🔒 100% Private and Secure, No Spam
