
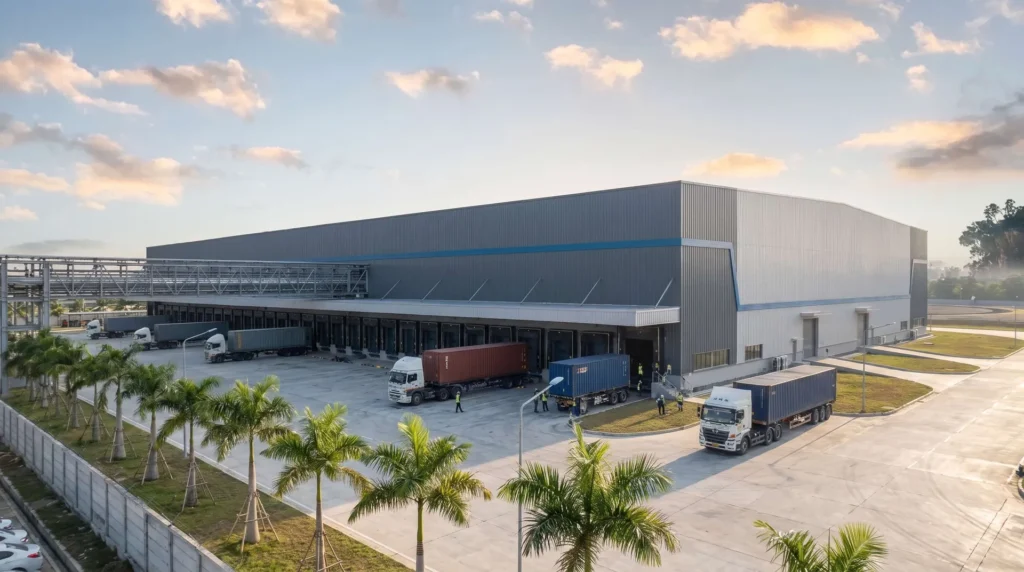
120,000 m² Modern EV Assembly Plant
Fabricated in Rayong Automotive Industrial Hub. Protective coating, bolted trial assembly. Handed over 24 Days Ahead of Equipment Fit-out.
Datos del proyecto
Los aspectos comerciales y técnicos que un contratista comprueba antes de solicitar los planos.
| Sector | EV Final Assembly & Battery Gigafactory |
|---|---|
| Ubicación | Rayong Automotive Industrial Hub, Thailand |
| Project Scale | 120,000 sqm Complex (~18,500 Tons Heavy Steel) |
| Diseño y ejecución | 100% Pre-Drilled Bolted Connections (0% Field Welding) |
| Delivery Result | Handed over 24 Days Ahead of Equipment Fit-out |
| Skybridge | Heavy tubular truss conveyor bridges (span up to 42m) |
| Nuestro ámbito de actuación | Fabrication, protective coating, bolted trial assembly and delivery |
Descripción del proyecto
How the structure was engineered, fabricated and delivered in Rayong Automotive Industrial Hub.
Located in the Rayong industrial corridor of Thailand’s Eastern Economic Corridor (EEC), this mega manufacturing campus serves as a flagship international production hub for next-generation electric vehicles and battery modules.
For the automotive client and EPC project management, the project schedule was non-negotiable—anchored to a global vehicle launch date and rigid Start of Production (SOP) milestones.
In the EV industry, missing the SOP deadline by even two weeks triggers tens of millions of dollars in lost market momentum, dealership breach penalties, and idle labor overhead.
Dimensions, codes, inspection rates and schedule outcomes for this project are recorded in the Project Facts table above, so they can be checked before an enquiry is issued.
Cuatro decisiones clave
Sub-Millimeter Deflection Skybridge Engine
Continuous spatial tubular truss skybridges engineered via dynamic FEA, holding high-speed conveyor live deflection under $\le 1/1200$ to prevent AGV and o
Solar-Optimized Reverse Precambering
Long-span roof rafters were pre-cambered using precision thermal and CNC cold-bending processes, offsetting dead-loads from rooftop solar panels and HVAC l
Zero-Hot-Work Battery Shop Clean Assembly
High-precision multi-spindle CNC drilling guaranteed 100% bolt alignment aloft, eliminating on-site cutting torches and weld spatter near cleanroom panels
Crane-Synchronized 3D Container Staging
Sequenced structural members into 40HQ containers strictly by building bays, allowing crawler cranes to lift directly from the haul road without double-han
El proyecto construido
Obras finalizadas, detalles estructurales y el equipo de ejecución en la obra.


Testimonio del cliente
Comentarios del cliente recogidos tras la entrega.
Missing our EV SOP launch window meant millions in losses. Shijie eliminated all risk: the 42m conveyor skybridge bolted into place with zero deflection, overhead solar roofs drained bone-dry during monsoon storms, and 18,500 tons of steel went up with zero torch cuts. Delivering 24 days early secured our global vehicle launch.
Preguntas frecuentes
Preguntas que se plantean los ingenieros antes de comprometerse con un proyecto de este alcance.
What was the structural scope of this EV gigafactory in Rayong?
About 18,500 tons of heavy steel across a 120,000 sqm campus: long-span final assembly halls, 42 m tubular truss conveyor skybridges linking the body and battery shops, and a roof structure engineered for a full rooftop PV array.
How do you keep a 42 m conveyor skybridge stable enough for automated transport?
The skybridges are continuous spatial tubular trusses analysed with dynamic FEA, holding live-load deflection within L/1200. Low-friction Teflon slide bearings at each expansion tier release thermal creep and vibration, so the conveyor line stays aligned at +40°C.
Rooftop PV adds dead load and monsoon rain adds ponding risk. How is that handled?
Primary roof girders are reverse-precambered in the shop to offset the PV dead load of at least 0.35 kN/m2, and the envelope uses a 360-degree double-lock standing seam roof rated above 160 mm/h rainfall, with fastener spacing set for uplift.
The battery shop cannot tolerate hot work. Is zero-welding realistic at that height?
Yes. Multi-spindle CNC drilling guaranteed bolt alignment on members erected 20 m up, so there was no site cutting torch, no grinding and no weld spatter anywhere near the battery areas. The clean-assembly requirement drove the detailing from day one.
How did you protect the Start of Production date?
Bays were pre-assembled on the ground and shipped in 40HQ containers sequenced strictly by building bay, so crawler cranes lifted directly from the container instead of a laydown yard. The steel package was handed over 24 days ahead of equipment fit-out.
Obtén tu presupuesto y plan de costos en 24 horas
Descubre cuánto puedes ahorrar en tonelaje de acero y en flete marítimo antes de que comience la fabricación
Reducción del peso del acero
El modelado 3D 1:1 de Tekla optimiza las relaciones viga-columna para eliminar los costos de material redundante.
Verificación de código sin conflictos
Se ha verificado de acuerdo con la norma EN 1090 y las cargas eólicas y sísmicas locales.
Revisión de ingeniero a ingeniero
Verificado por nuestros ingenieros principales: sin llamadas de ventas agresivas, solo datos útiles y precio de fábrica.
CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001
Ingenieros principales en línea
🔒 100 % privado y seguro, sin spam